The line your product is actually built on.
We do not hand your design to an unknown third party. Boards are placed and reflowed, cases are moulded or machined, finishes are applied and units are aged and tested on production lines we control and audit ourselves — from a first prototype through to a full container.
- SMT, injection, CNC, PVD finishing and final assembly under one production plan
- 100% functional test on every unit, plus AQL 2.5 final inspection
- Tooling, firmware and quality records kept under our own process control
- Buyer and third-party audits arranged on request
Site documentation, capacity statements and current audit reports are shared during supplier qualification.
| Location | Shenzhen · Dongguan Guangdong, China |
|---|---|
| Production area | 12,000 m² assembly, tooling, finishing |
| SMT lines | 4 high-speed lines in-line 3D AOI |
| Assembly cells | 6 cells watch, band and ring builds |
| Monthly capacity | 300,000 pcs across all three platforms |
| Quality system | ISO 9001 certified 100% functional test · AQL 2.5 |
| Audits | Buyer and third-party audits arranged on request |
What is actually on site.
Everything a wearable needs happens inside the same plan: electronics, mechanics, finishing, assembly and test. That is what lets a specification change move through a quotation in days rather than weeks — and what makes a defect traceable back to the batch that produced it.
Vertical scope
- PCB assembly — placement, reflow, in-line AOI and board-level functional test
- Tooling — injection moulds for cases and straps, CNC for titanium ring bodies and stainless cases
- Surface finishing — PVD, electroplating, spray and laser marking
- Display lamination and full-module bonding
- Final assembly, aging and packing, including retail-ready boxes
Site figures
- Production area
- 12,000 m²
- Production staff
- 260
- Engineering staff
- 35
- Shifts
- 2 shifts, 6 days
- Sample shop
- On site — CNC and 3D printing
- Warehouse
- Finished goods and components, separate zones
Site figures are stated as at the last internal audit. Capacity, headcount and certification copies are provided in the supplier qualification pack, under NDA where required.
Six stages, and what gets checked at each one.
A defect caught at stage two costs a fraction of the same defect caught after packing. This is why the checks sit inside the flow rather than at the end of it.
-
STAGE 01
Incoming material & IQC
Every lot of cells, displays, sensors and plastics is inspected on receipt against the approved specification. Non-conforming lots are quarantined and reported, not quietly consumed.
-
STAGE 02
SMT & board-level test
Placement and reflow on high-speed lines, in-line 3D AOI on every board, then a board-level functional test before the board is released to assembly.
-
STAGE 03
Tooling & sub-assembly
Moulded or machined parts are checked against the golden sample, finished, then fitted to the board with the display laminated and sealed.
-
STAGE 04
Assembly & functional test
Final assembly, then a full functional test on every single unit — sensing, screen, touch, charging, radio and water-resistance sampling.
-
STAGE 05
Aging & reliability
48-hour burn-in on production samples, plus thermal cycling and drop testing per programme. Failures here send the batch back, not forward.
-
STAGE 06
Final QC, packing & shipment
AQL 2.5 inspection on the finished batch, third-party inspection if you want it, retail packing, carton sealing and shipment on your forwarder or ours.
Any batch that fails a stage is held and reported with an 8D corrective action. It does not ship with a note attached.
The workshop, not a render.
These are the actual stations a wearables order moves through. Panoramic frames are wide-angle; ask during a video or on-site audit for a live walk-through.
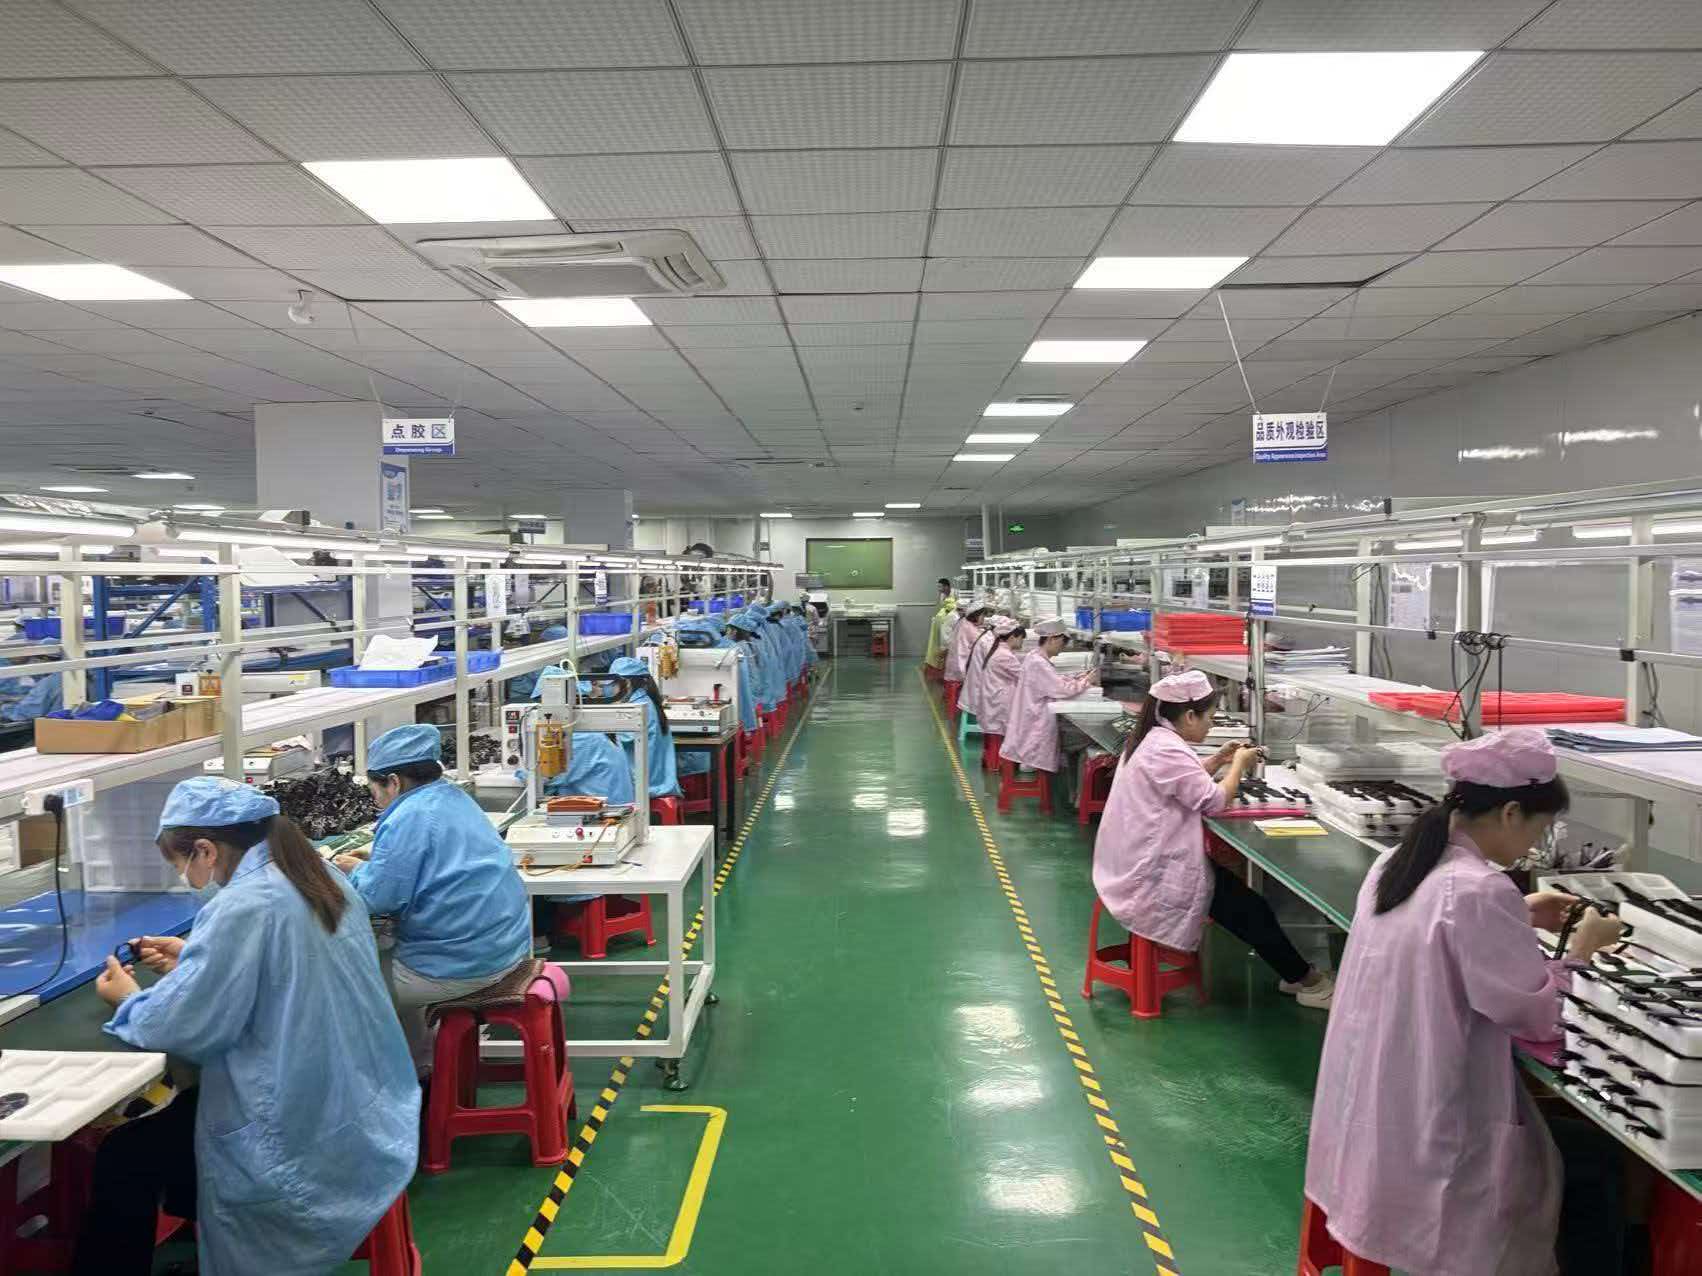
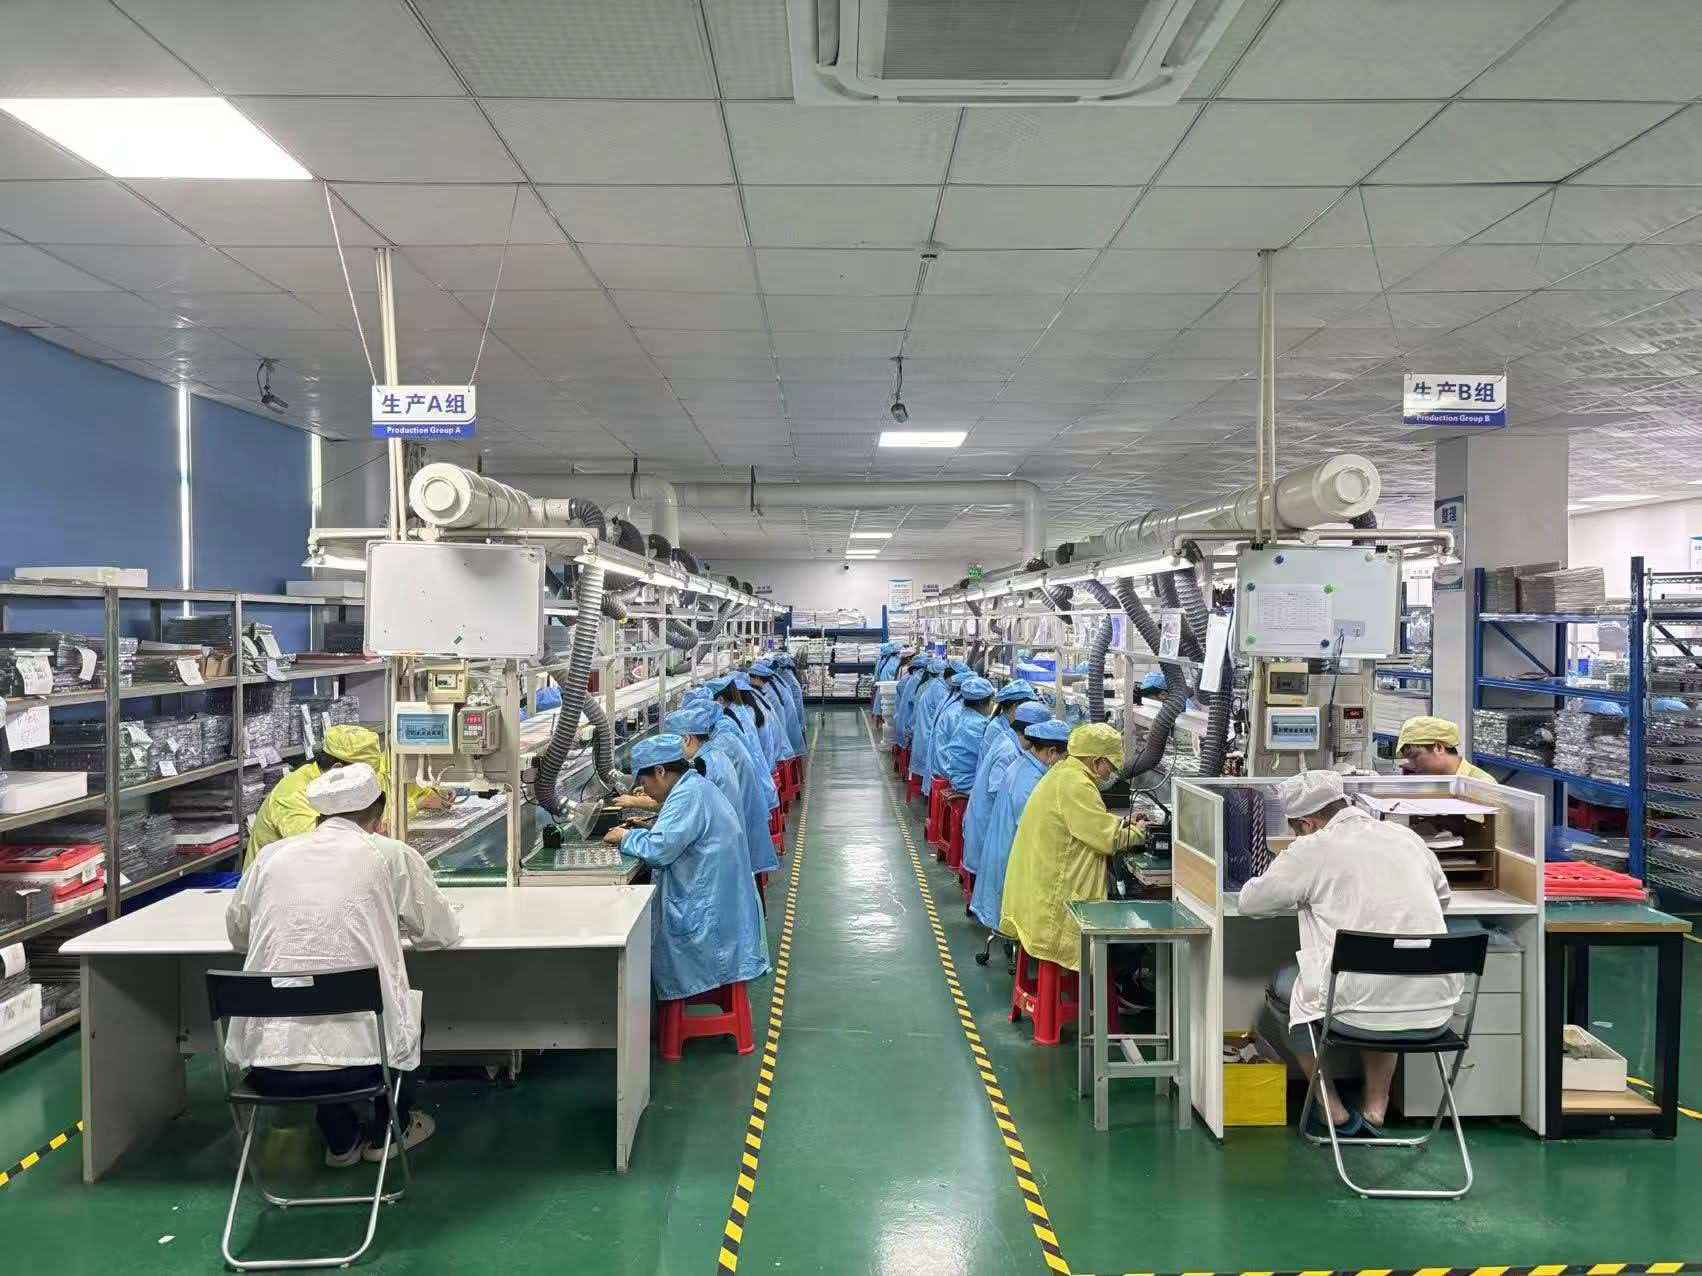
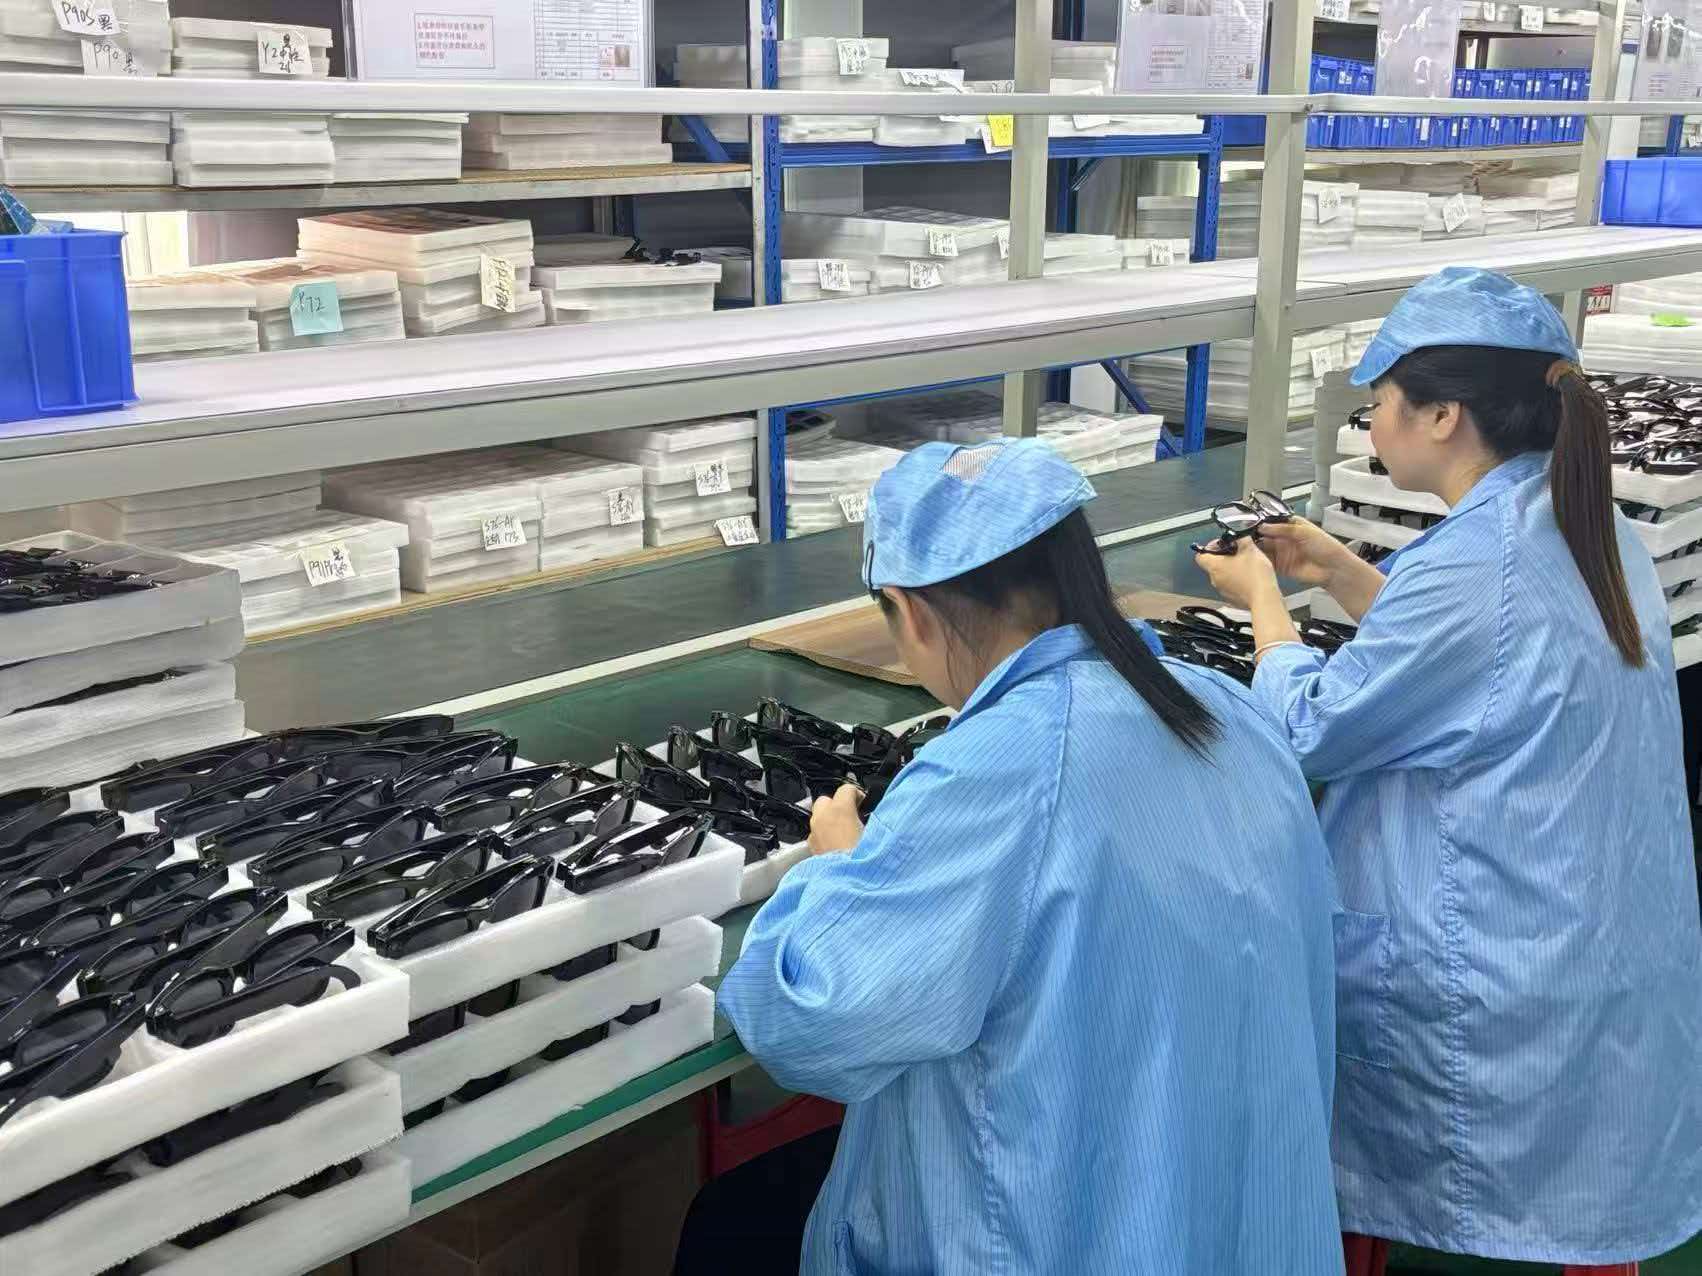
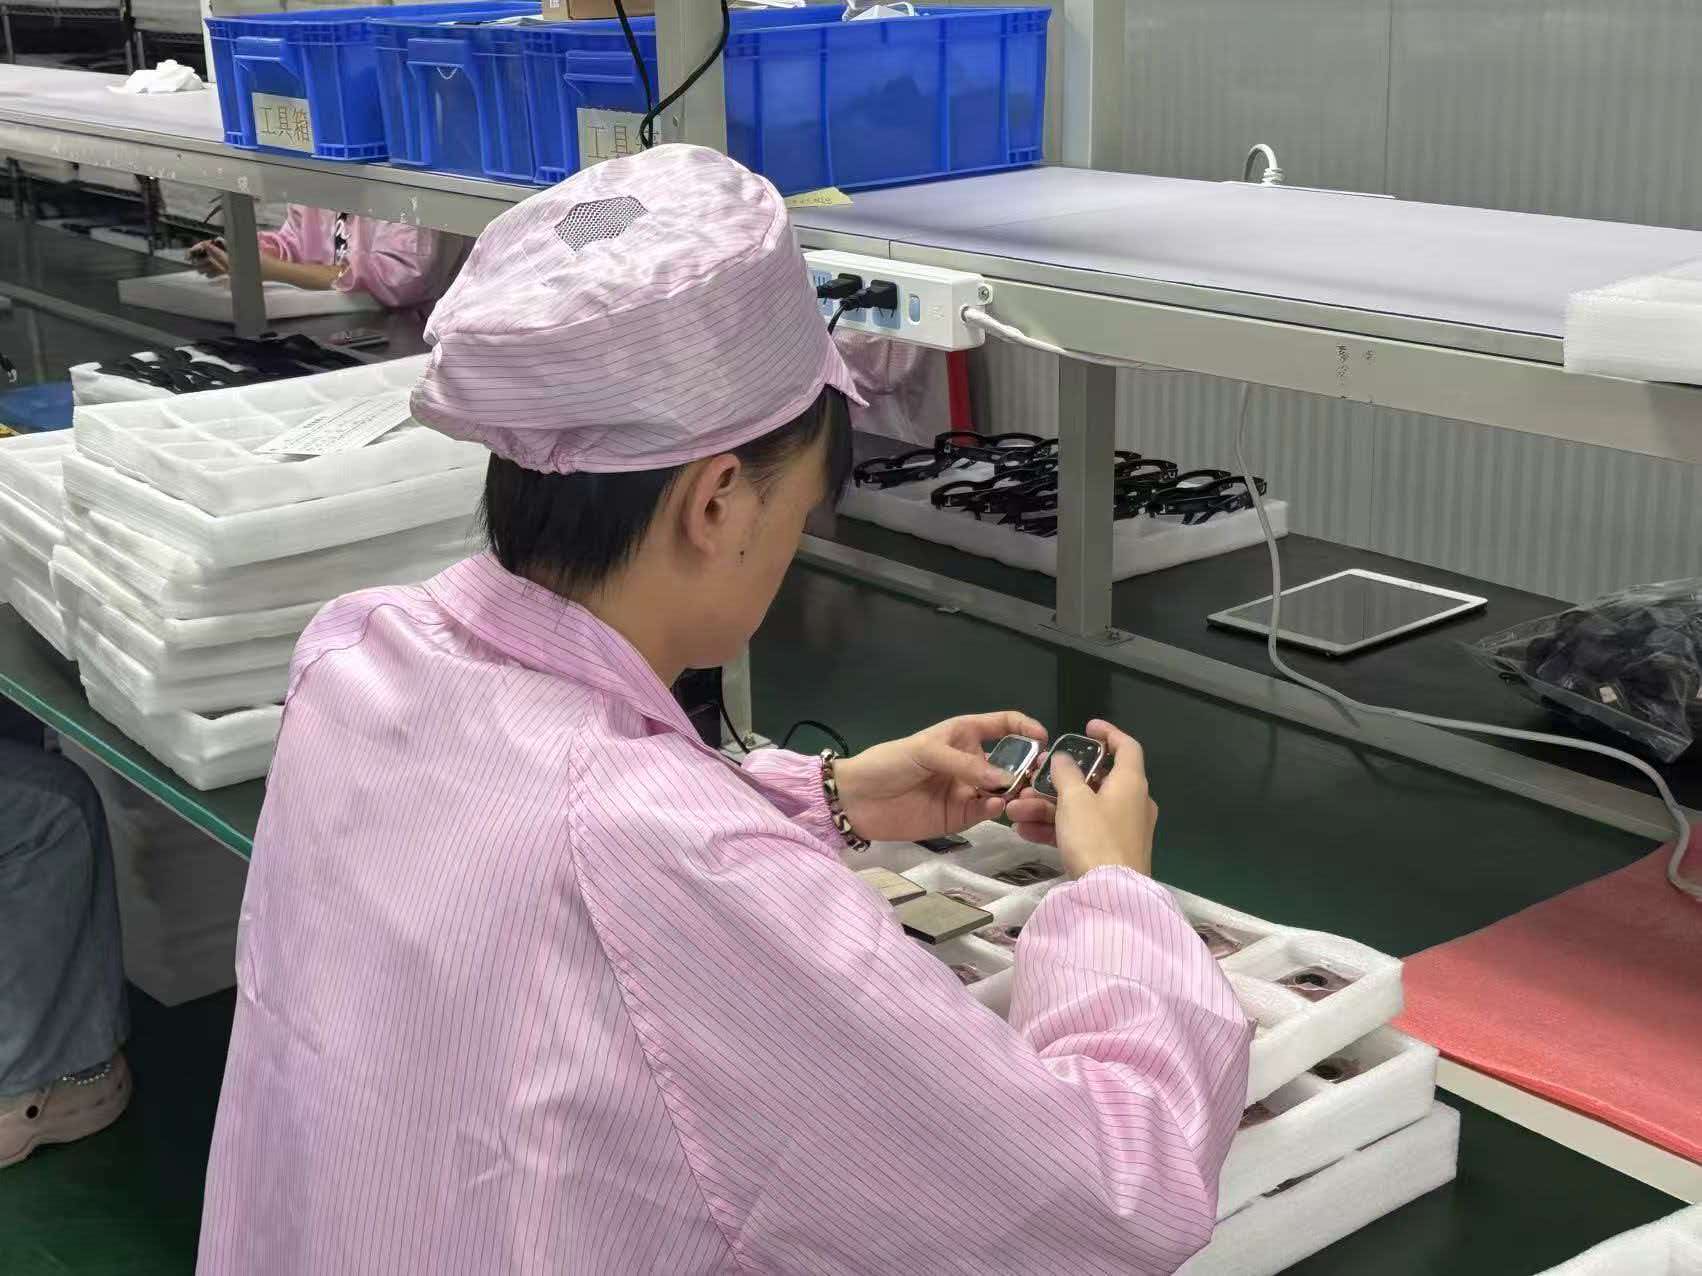
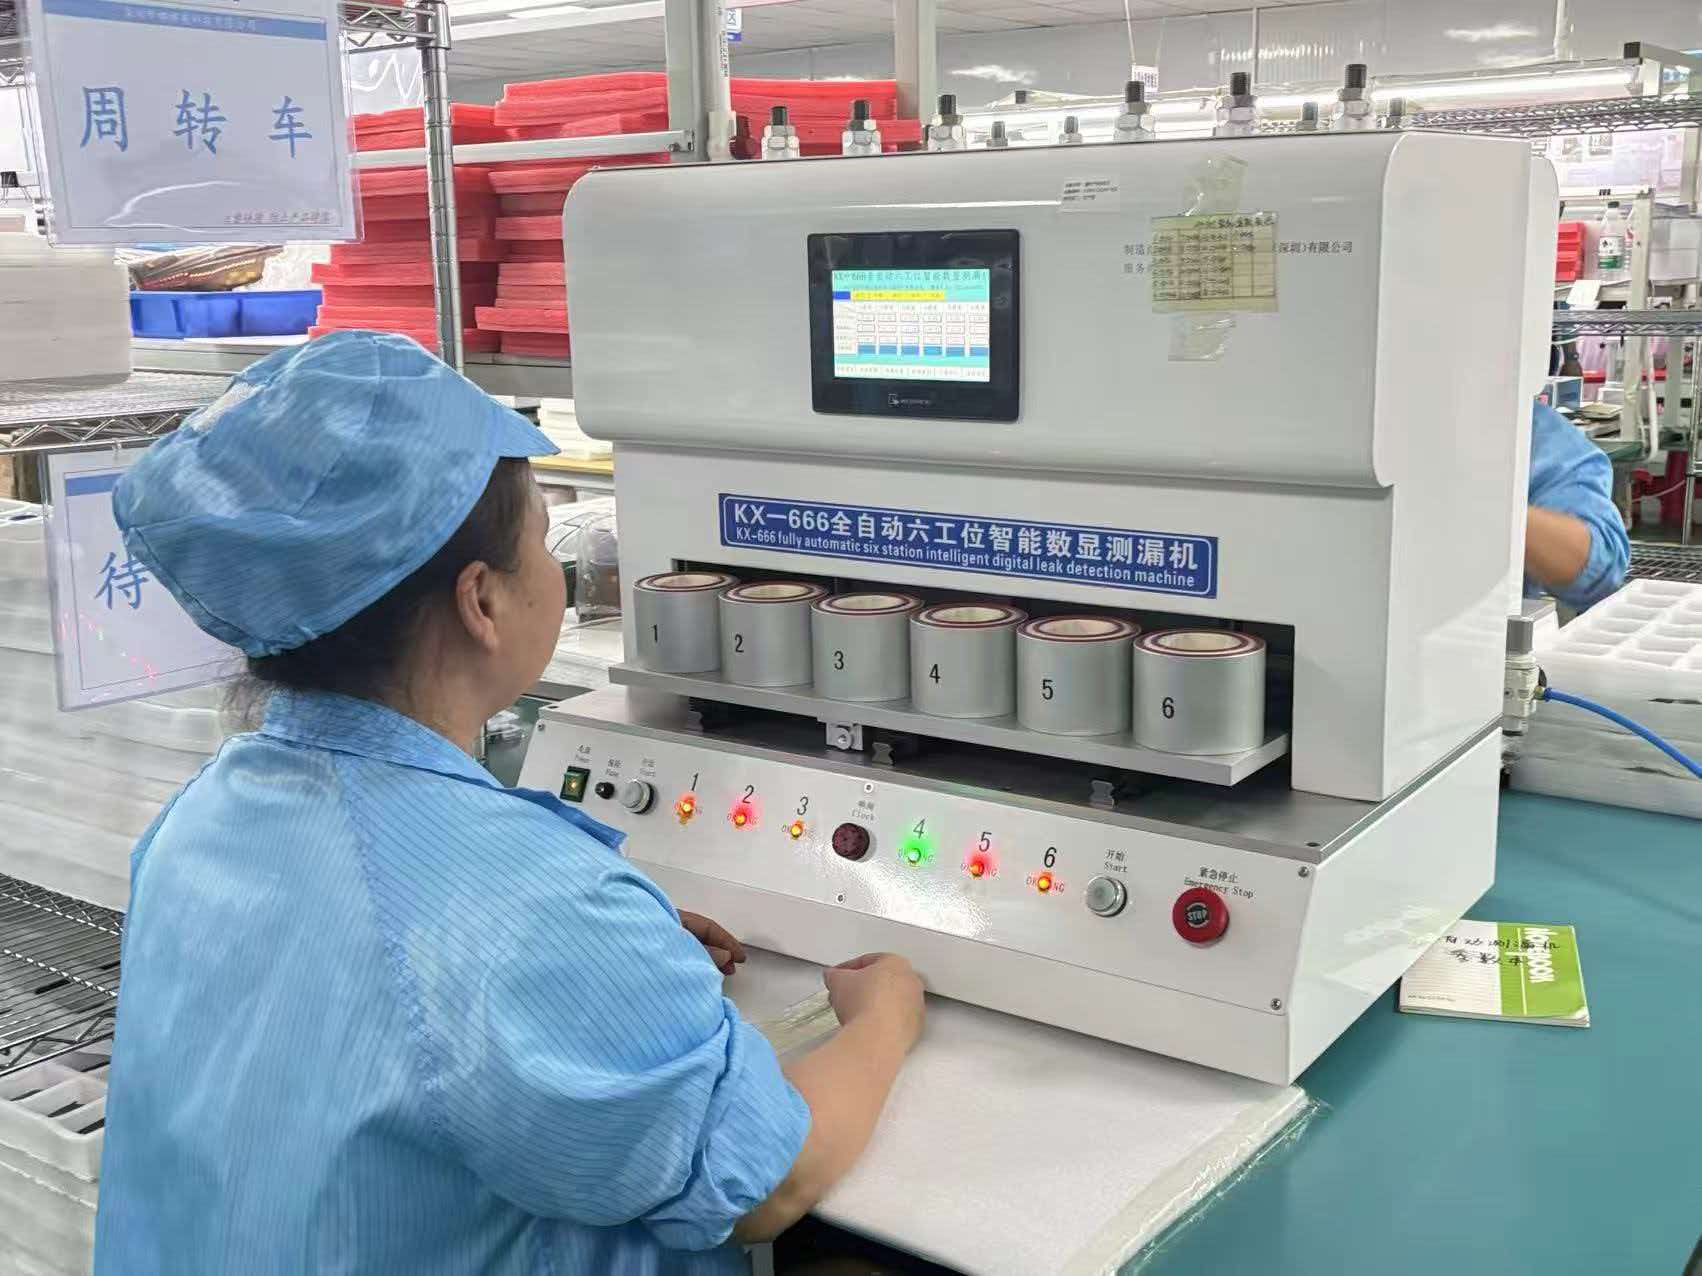
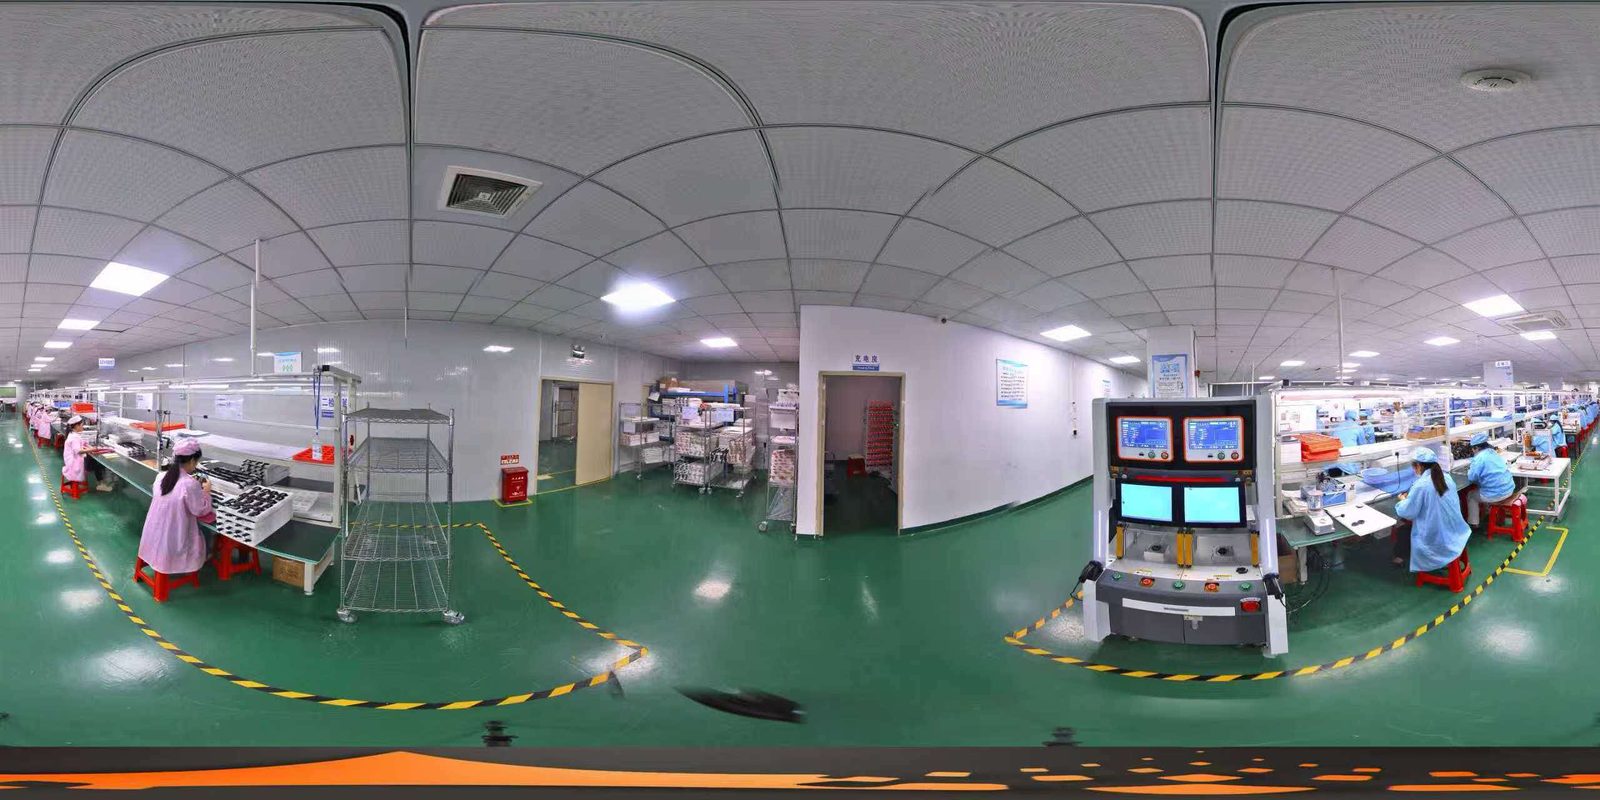
Photographs are un-staged production documentation. Machinery and line layout may differ from the allocation confirmed for a specific programme.
What the lines can actually do.
If your specification needs a process that is not on this list, say so early — we will tell you whether it is something we run, something we tool up for, or something you should not attempt on this platform.
| Process | Equipment | Capability |
|---|---|---|
| SMT placement | 4 high-speed lines | 0201 chip placement · combined 320,000 CPH |
| Reflow & AOI | 6-zone reflow ovens · in-line 3D AOI | Solder joint inspection on 100% of boards |
| Injection moulding | 12 machines, 60–180 T | Cases, straps and packaging inserts · in-house colour matching |
| CNC machining | 8 machining centres | Titanium ring bodies, stainless steel cases, tooling inserts |
| Surface finishing | 3 PVD and plating lines | Black, gold and rose-gold PVD · electroplating · laser marking |
| Display lamination | 3 laminating lines | Full lamination with per-lot yield reporting |
| Assembly | 6 assembly cells | Watch, band and ring builds, changeover per work order |
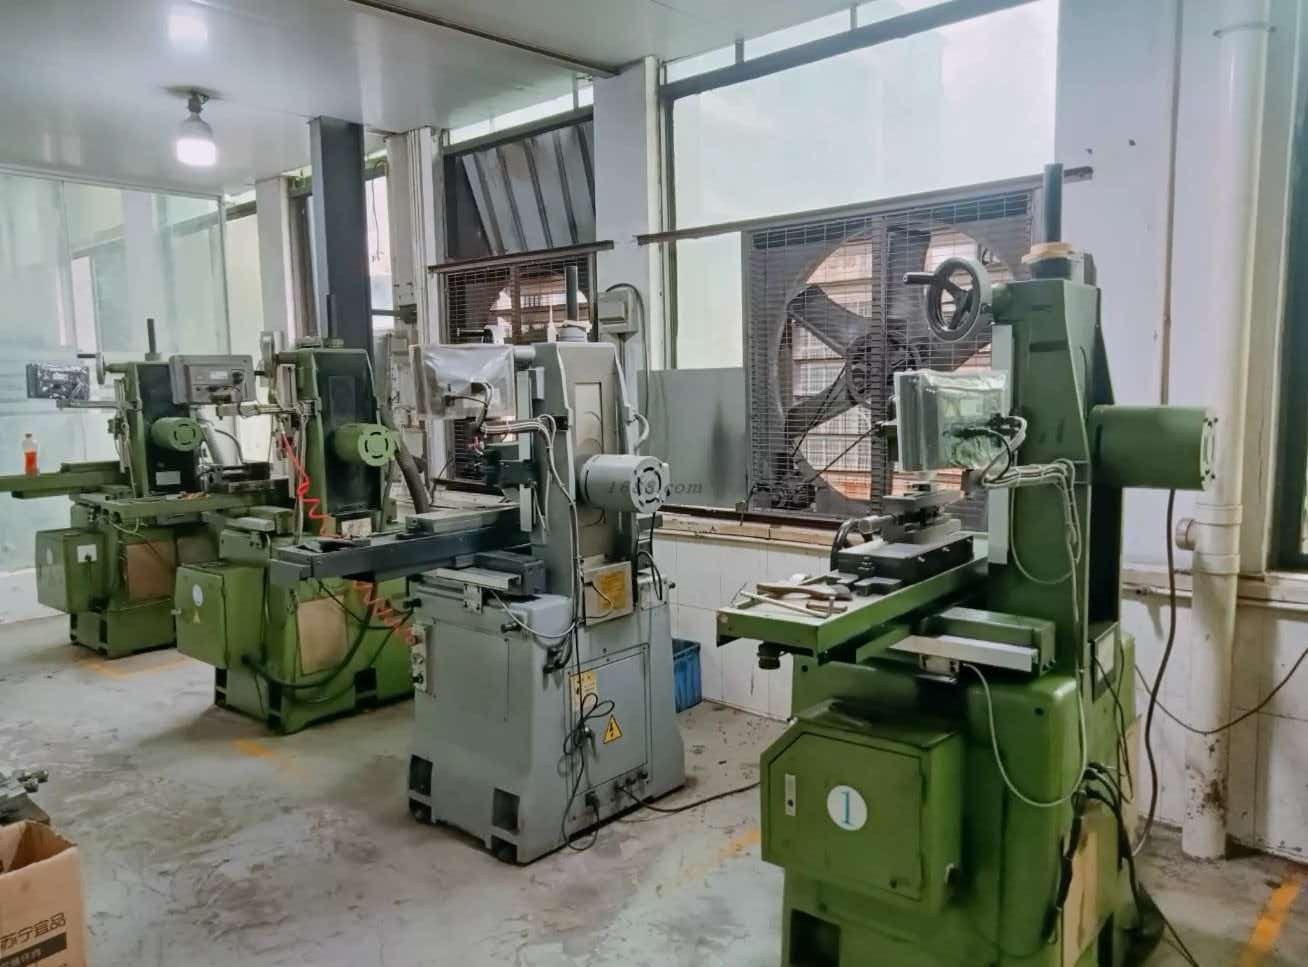
| Tooling & mould making | ZNC EDM spark machine · BF-650E CNC centre | In-house mould/electrode making and precision metal parts |
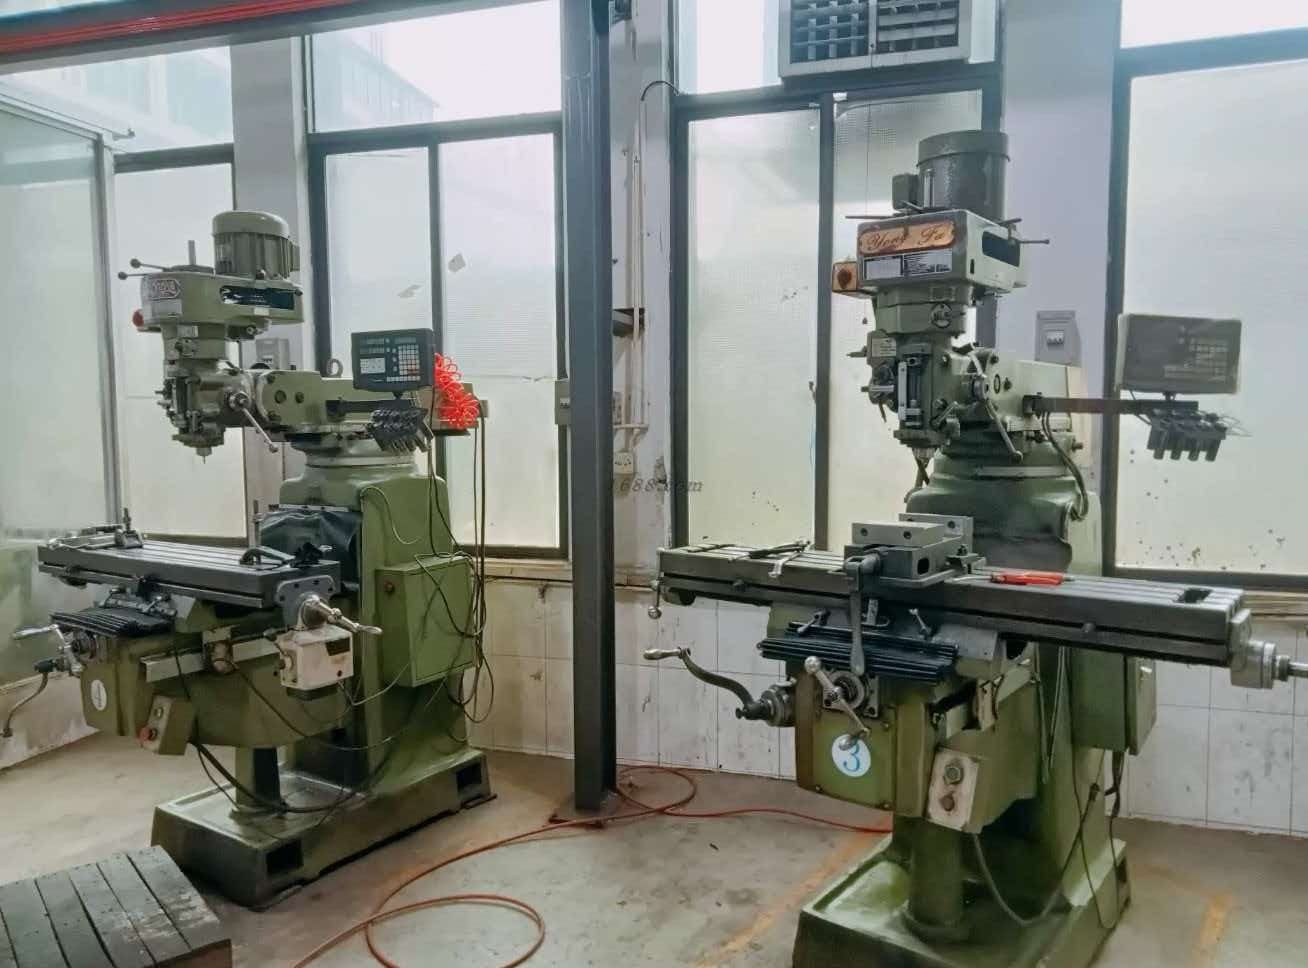
| Milling & surface grinding | 2 turret milling machines (3-axis DRO) · multiple precision grinders | Jigs, fixtures and tight-tolerance metal components |
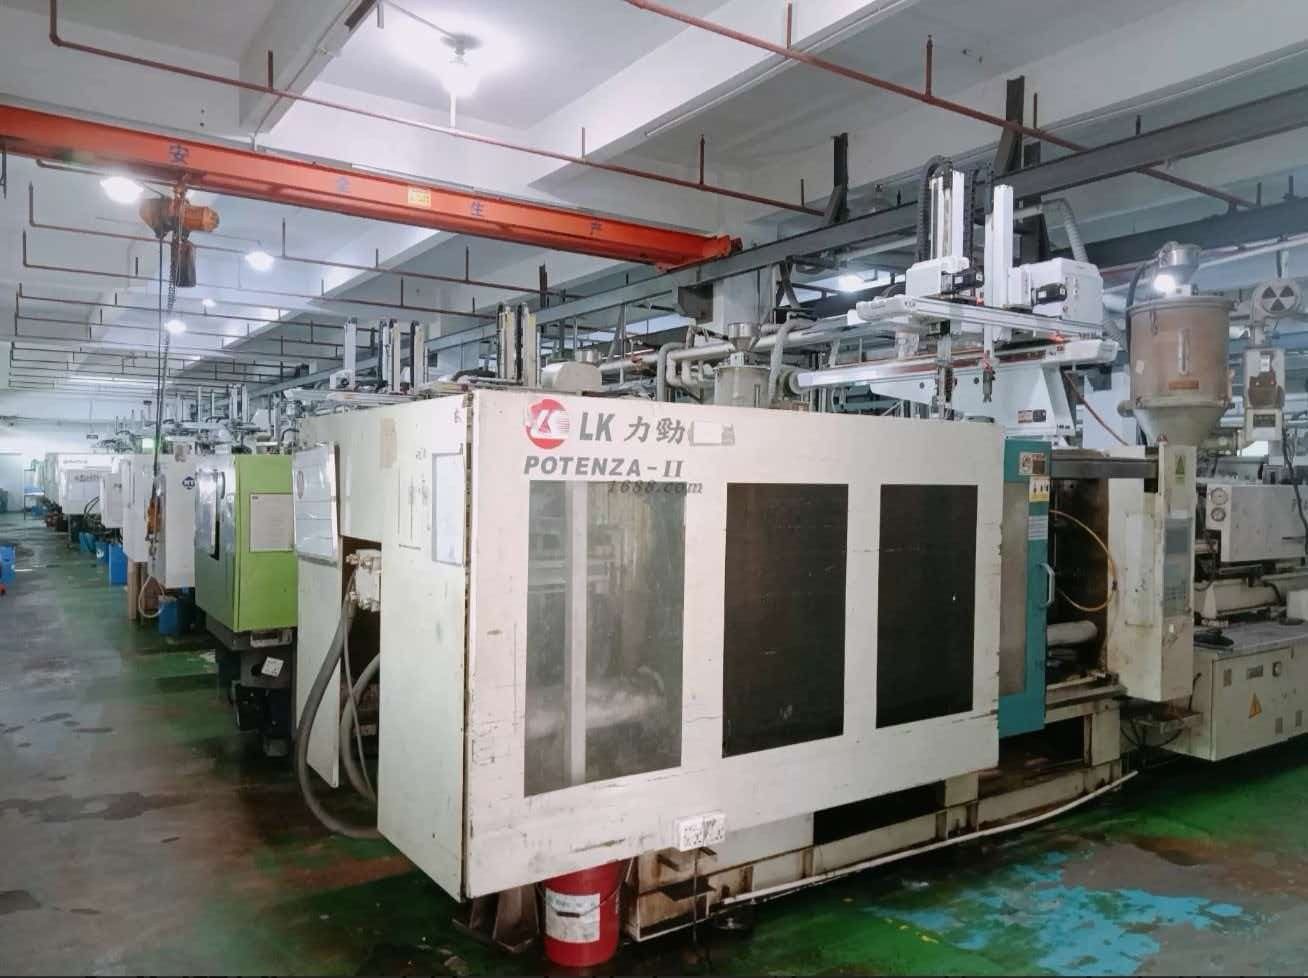
| Injection moulding | LK Potenza-II servo hydraulic presses (in-line robots) | Cases, straps, eyewear housings and packaging inserts |
| Battery grading | Multi-channel battery capacity separator / cycler | Cell capacity sorting and charge-discharge cycling before build |
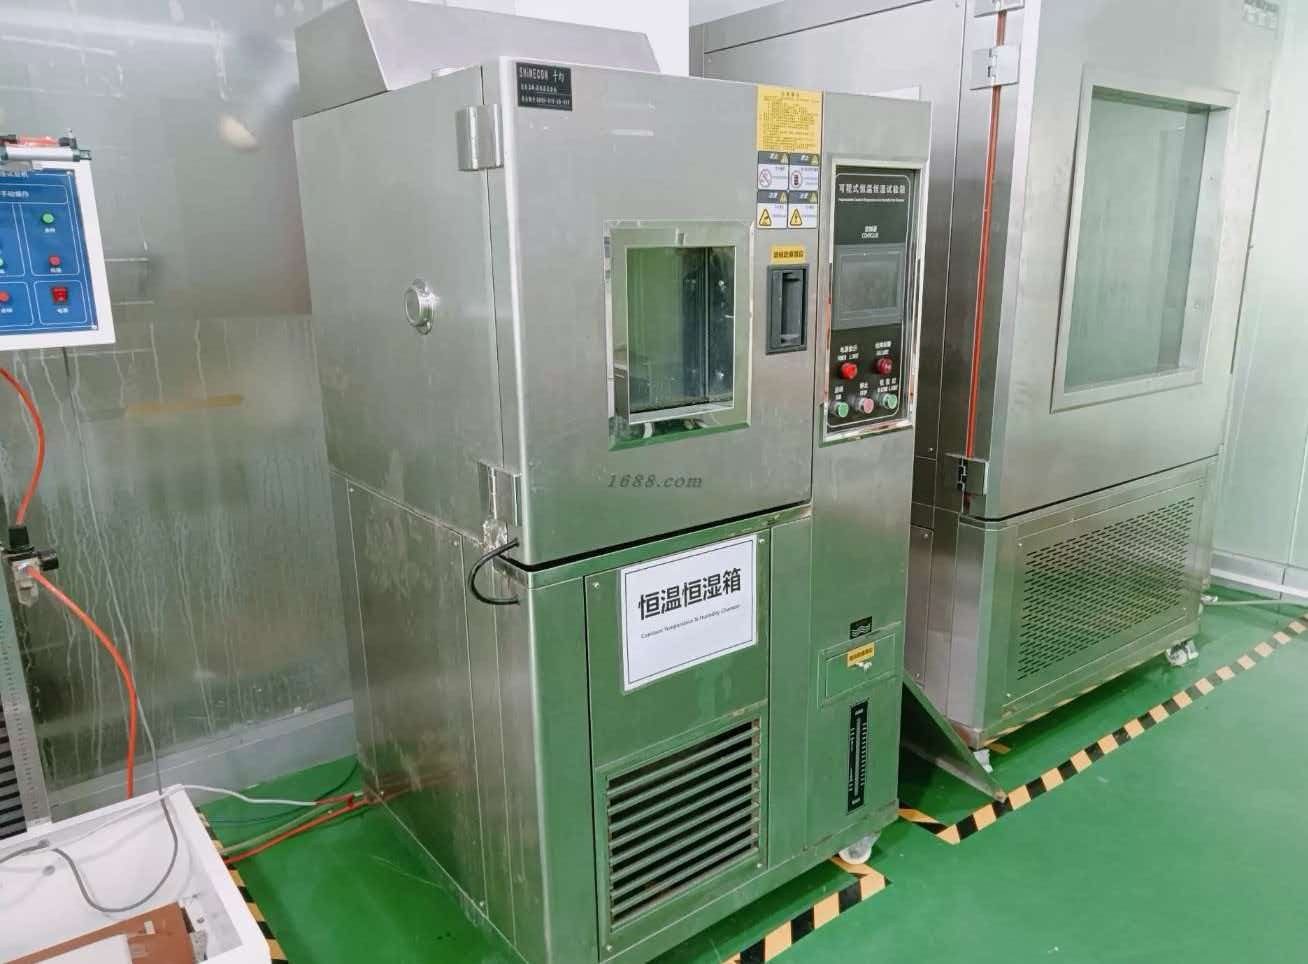
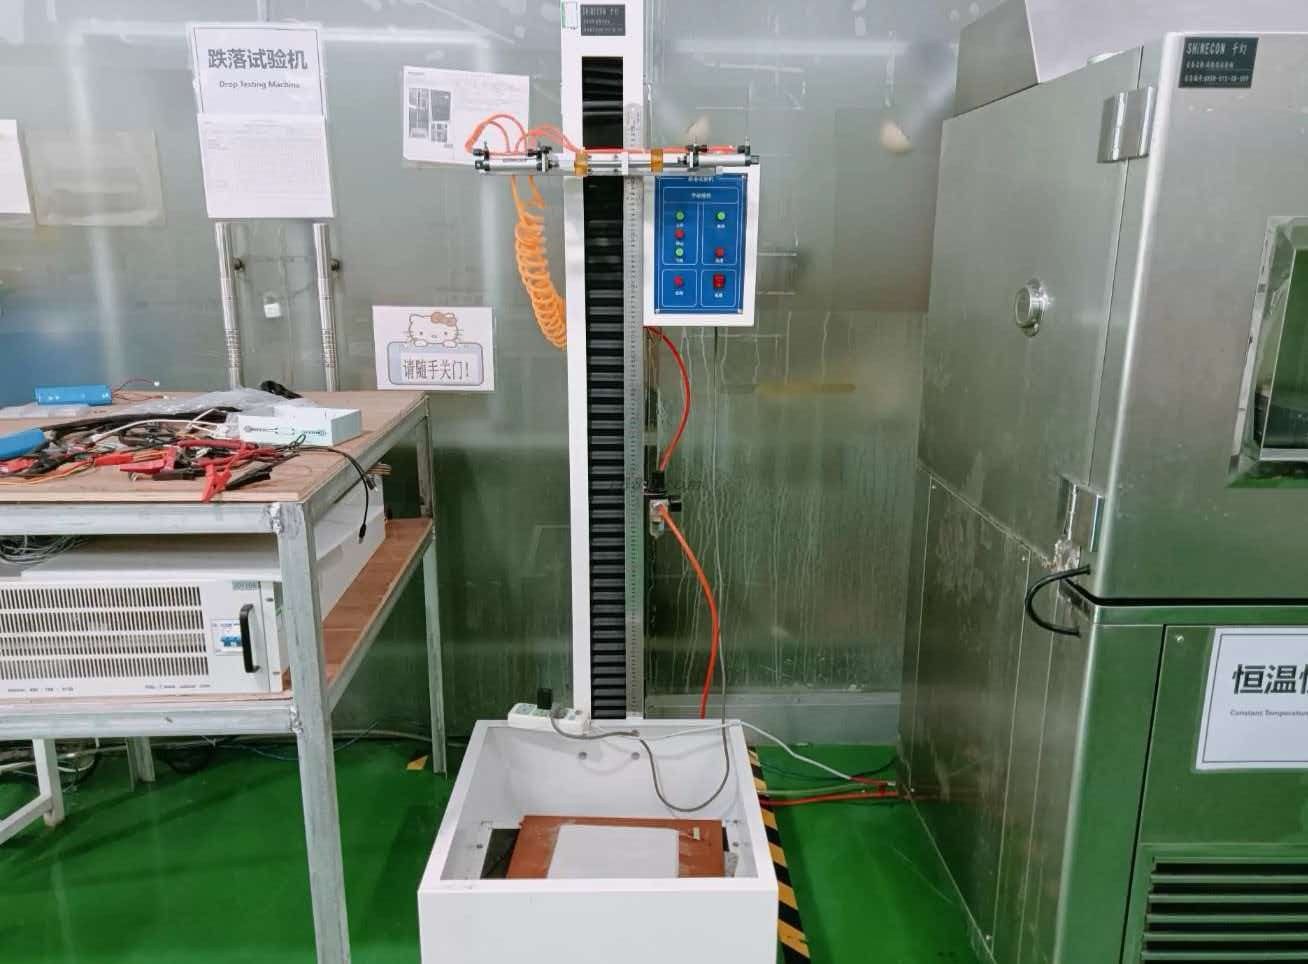
| Aging & reliability | 48 h aging racks · constant temp/humidity chamber · drop tester | Burn-in, thermal/humidity cycling and free-fall drop testing |
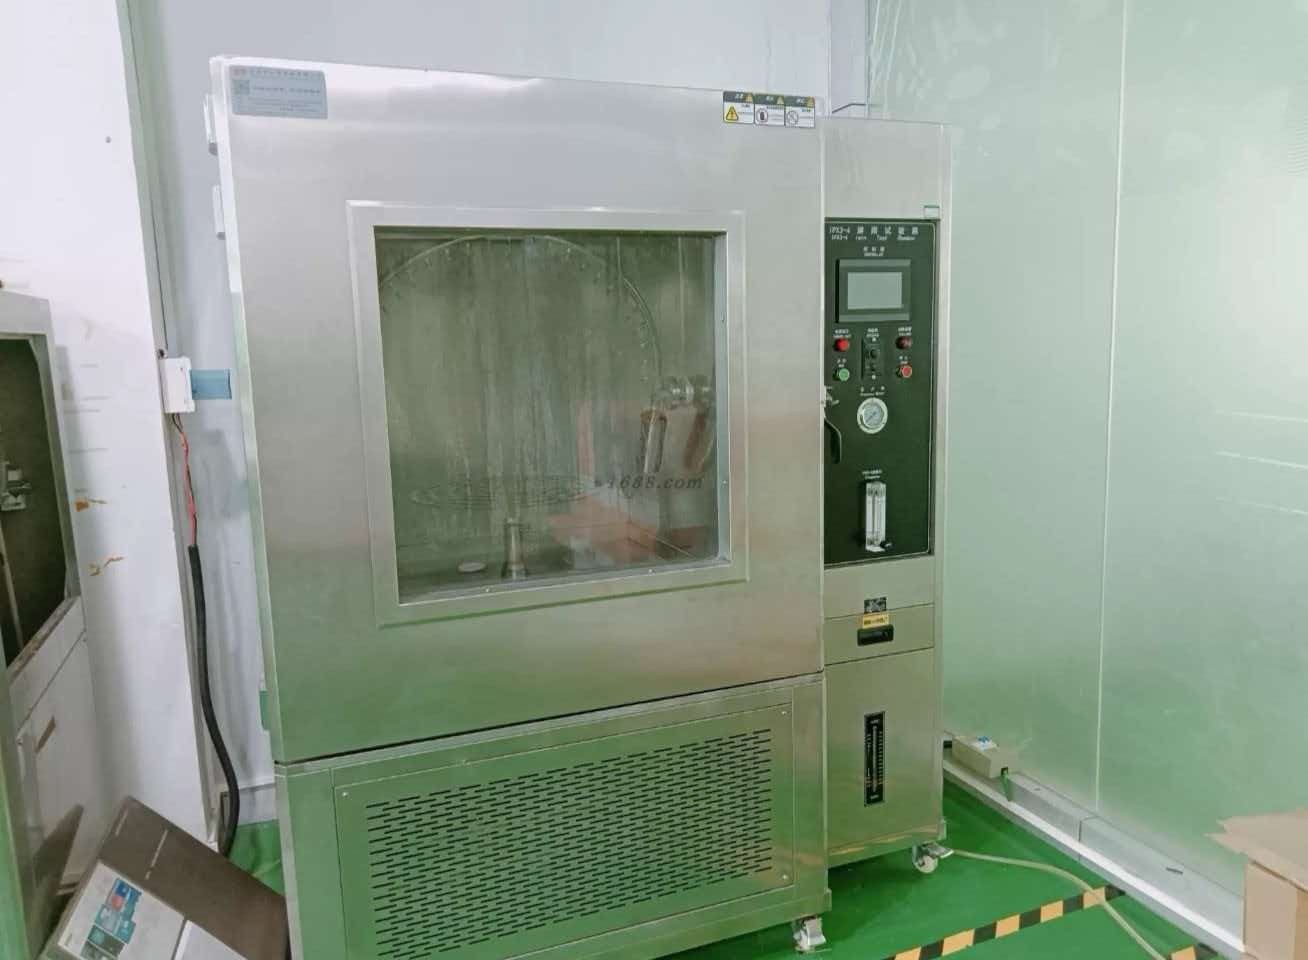
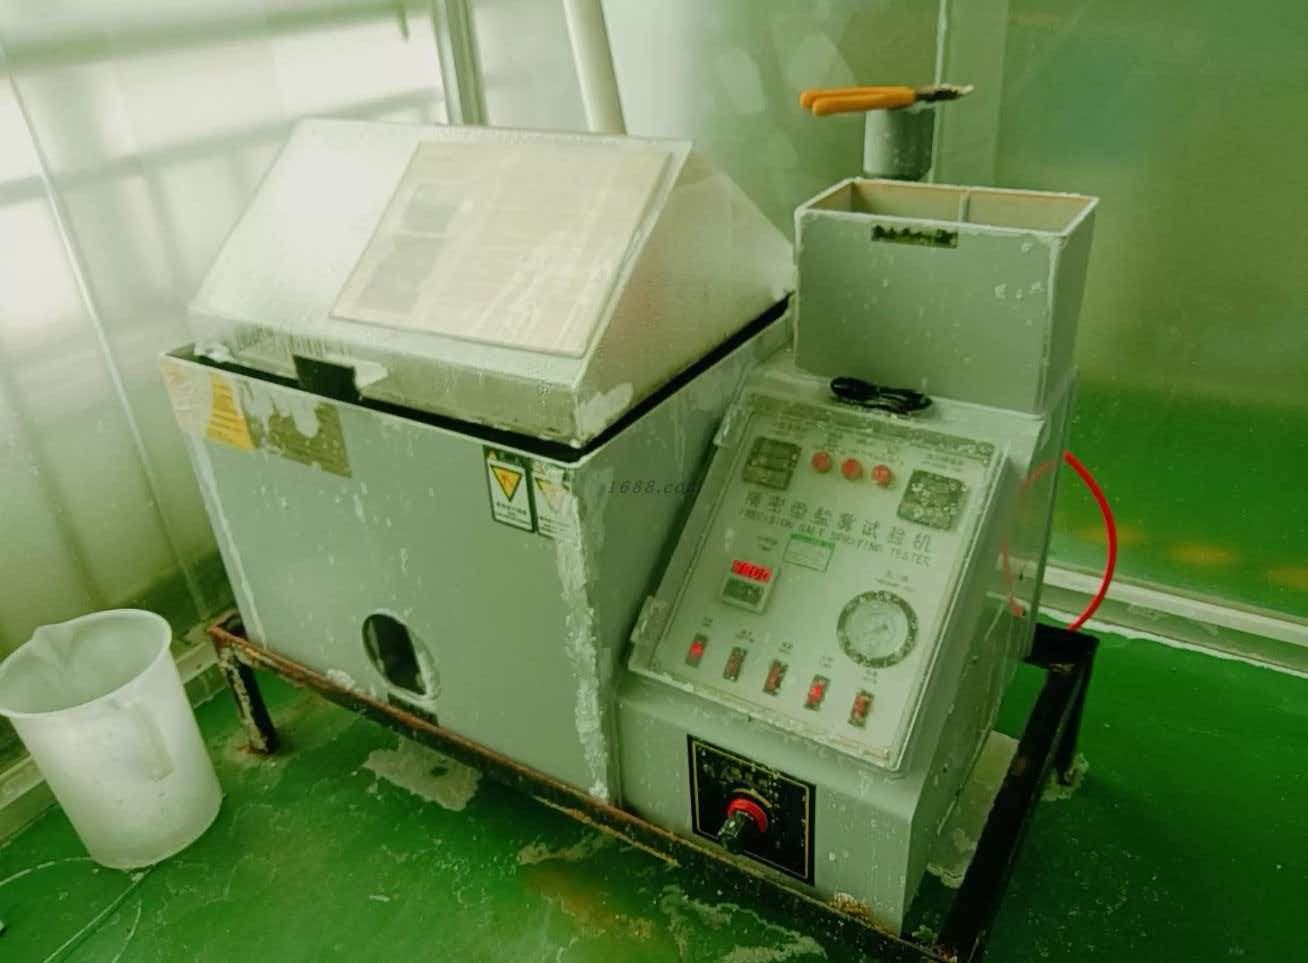
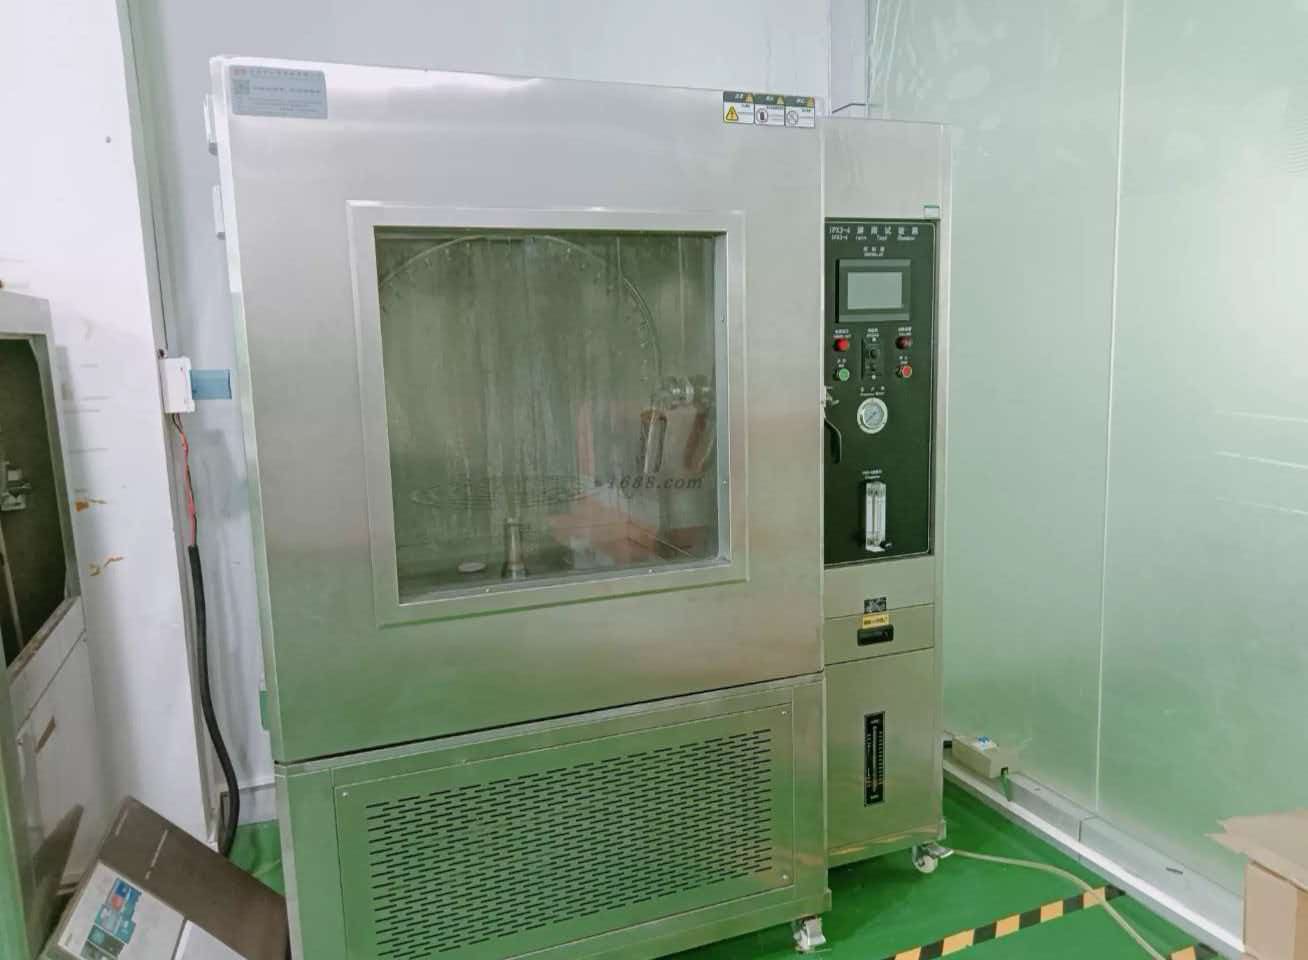
| Environmental & IP test | Salt-spray chamber · IPX rain/spray chamber · KX-666 leak tester | Corrosion, ingress and water-resistance verification |
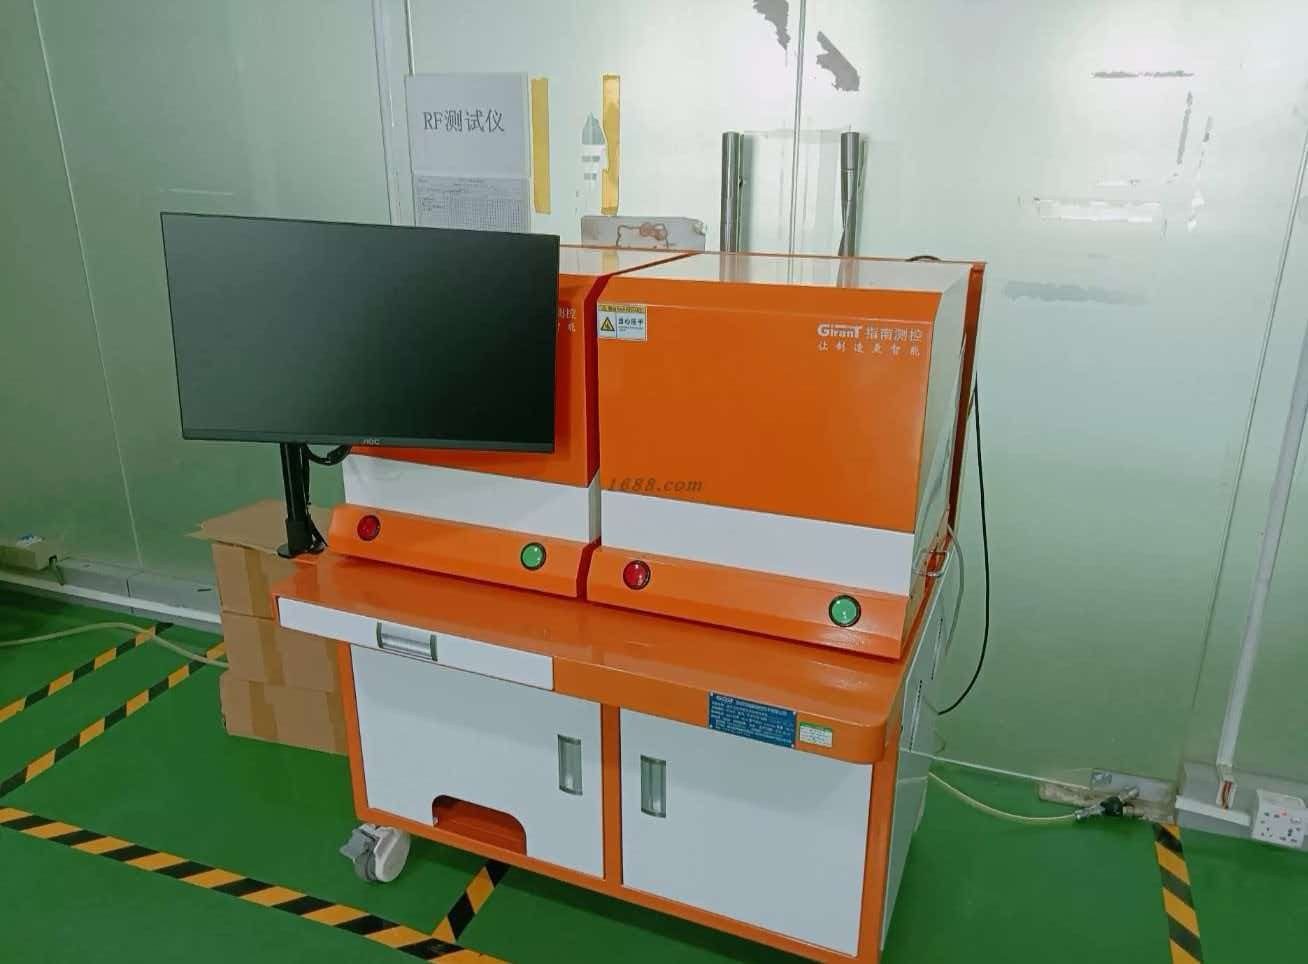
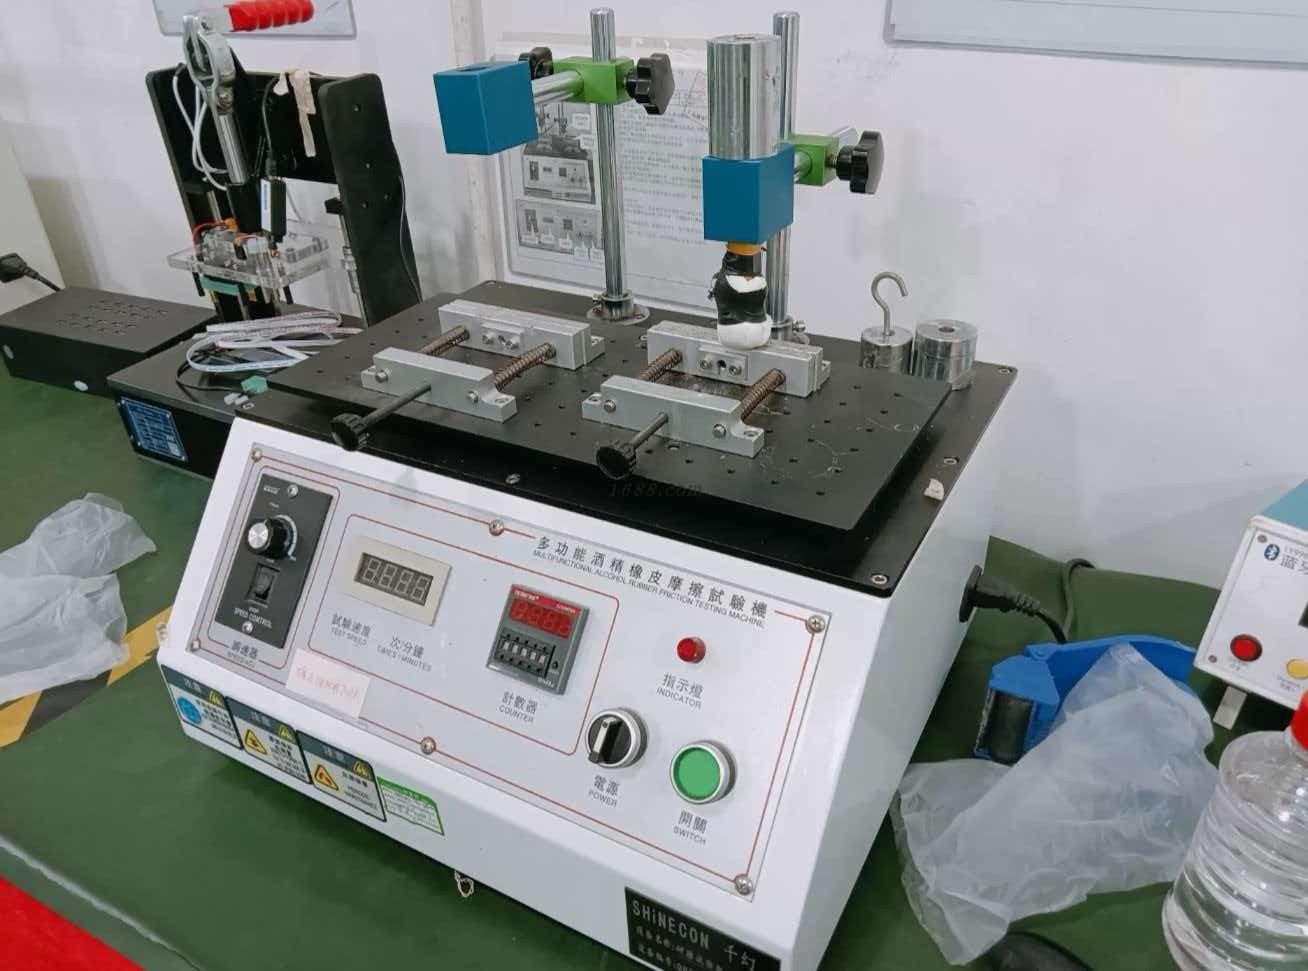
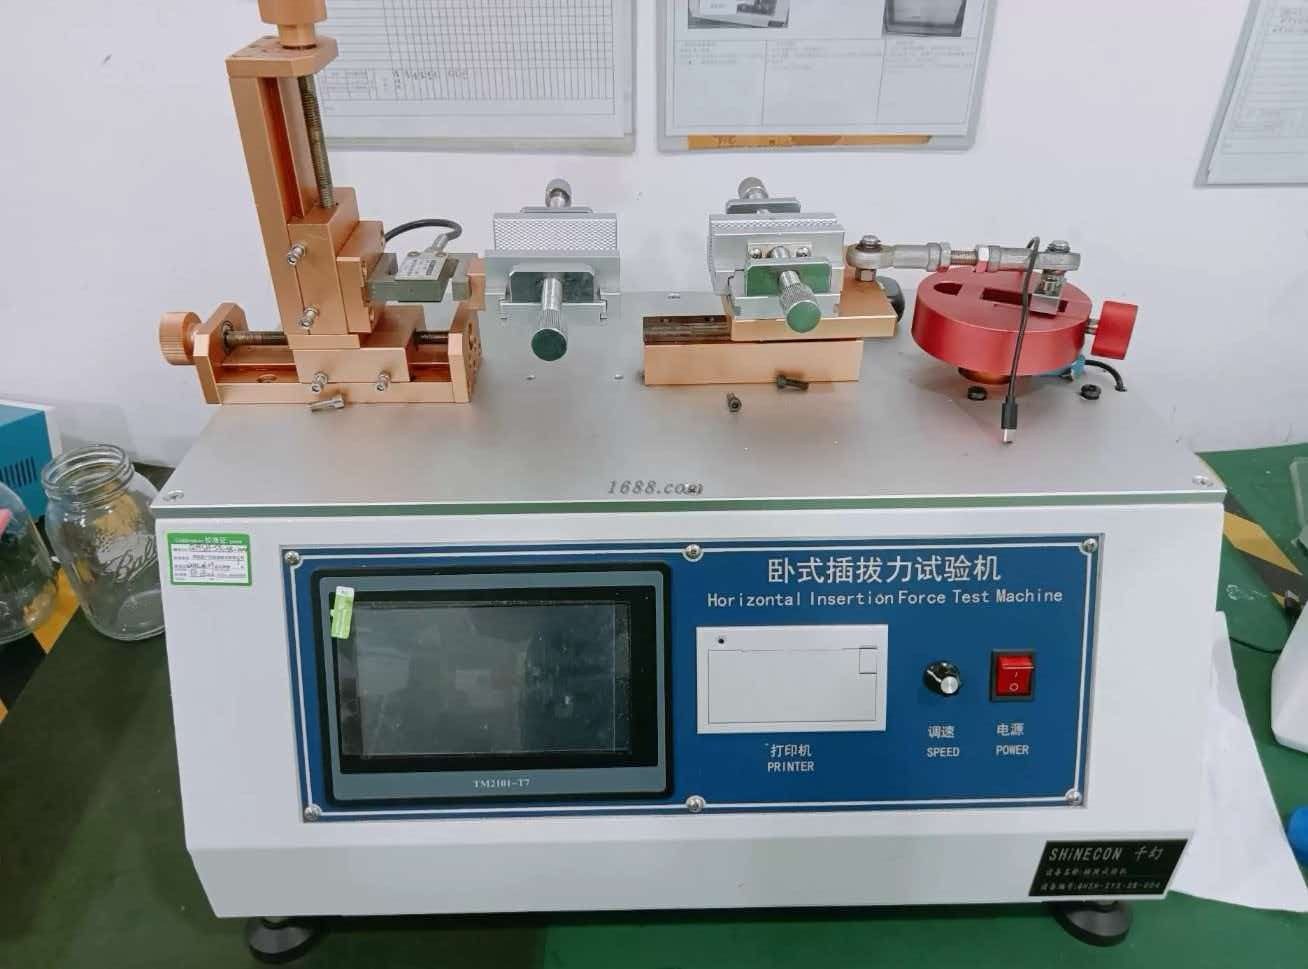
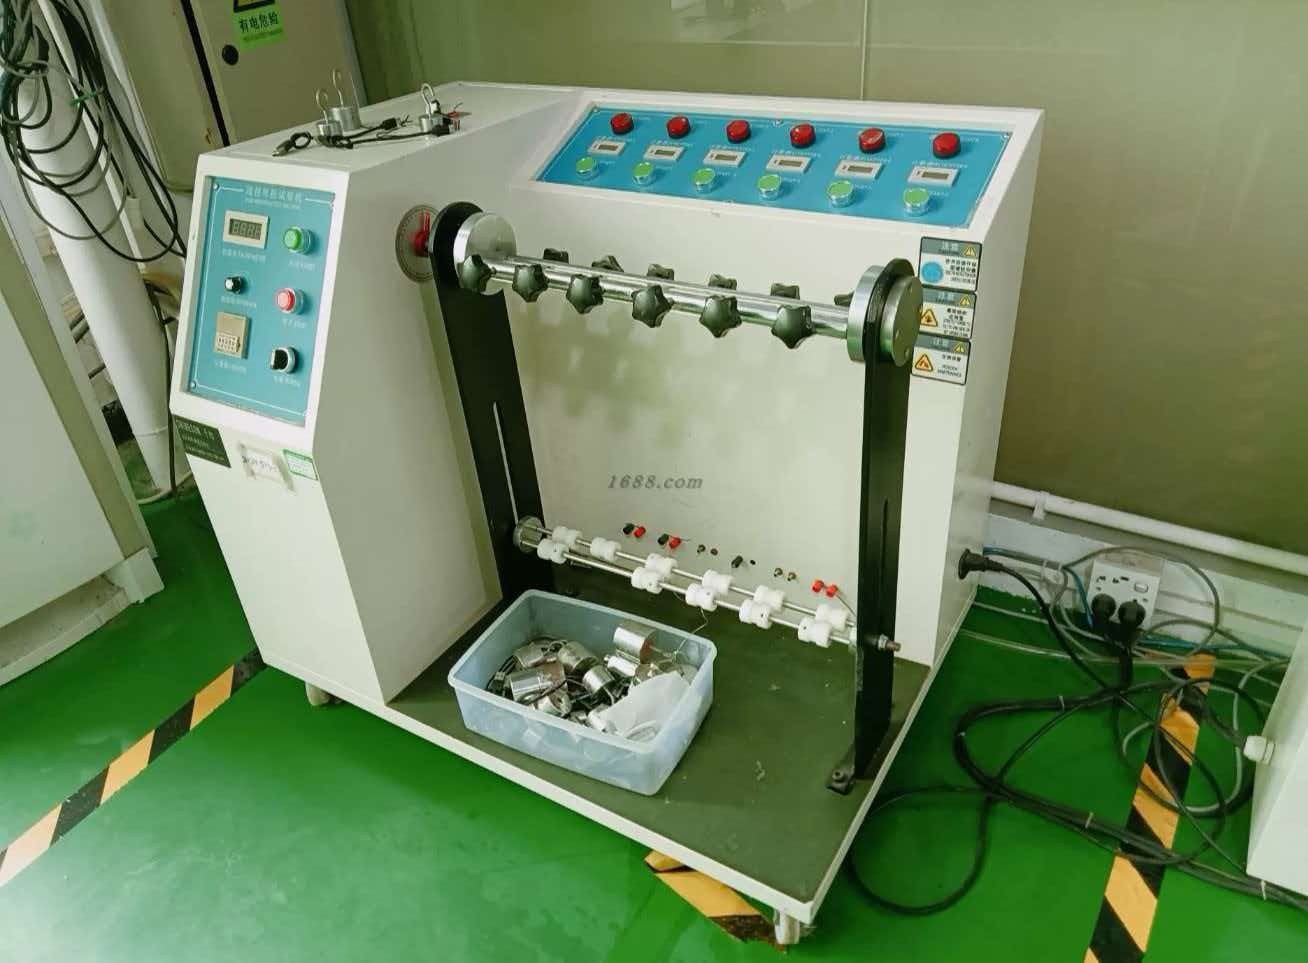
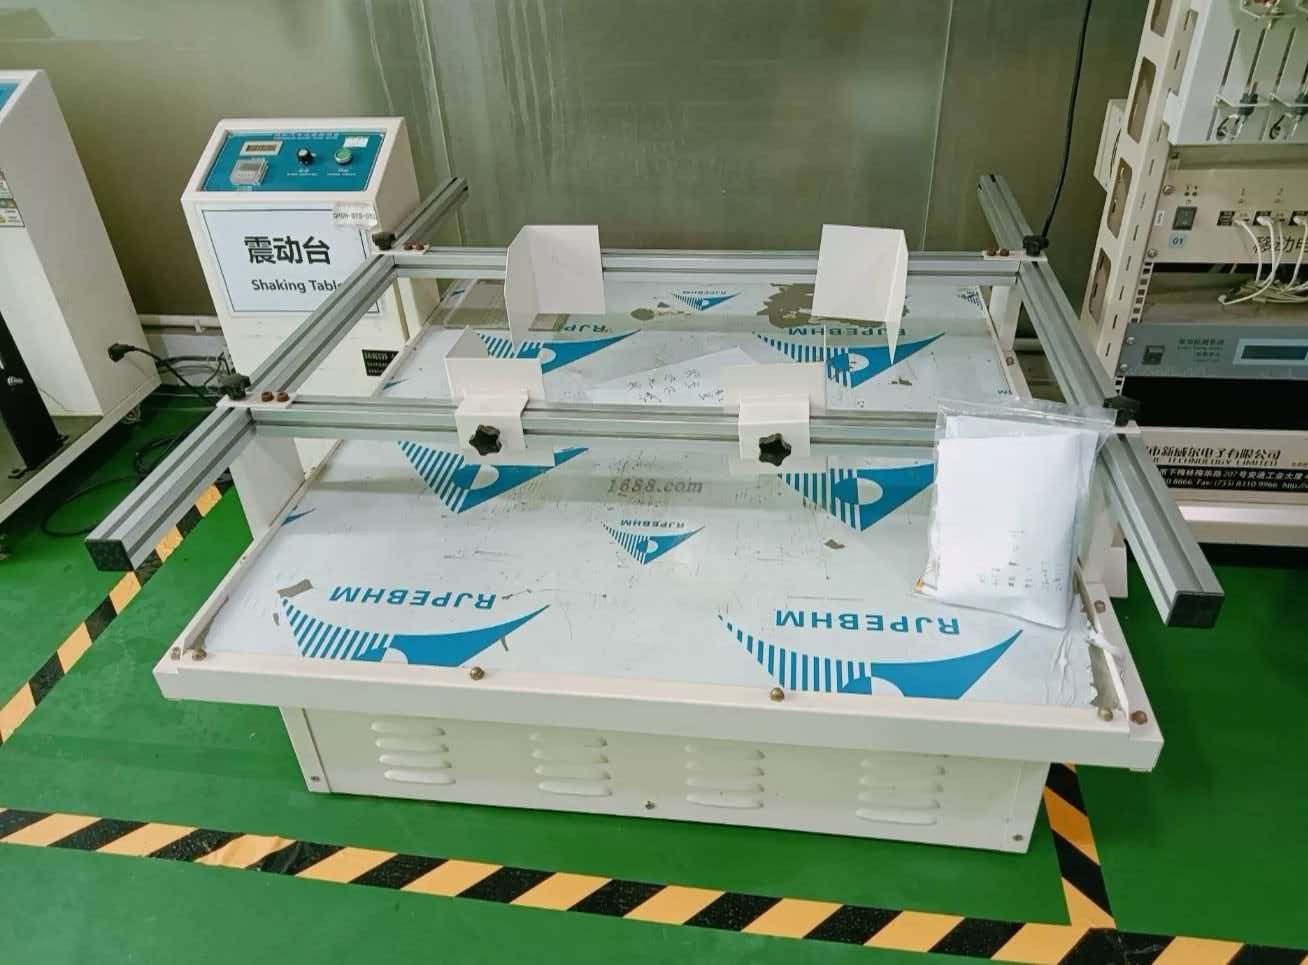
| Mechanical & RF test | Insertion/force tester · cable flex tester · vibration table · RF shielded tester · abrasion tester | Connector life, flex endurance, transport vibration, RF and surface wear checks |
| Functional test | Test benches · water-resistance tester | 100% functional test · IP and ATM sample verification |
| Packing | 2 packing lines | Retail box assembly, labelling, carton sealing, palletising |
Process capability is confirmed against your specification in the written quotation. Line allocation for a programme is agreed at order confirmation, not at enquiry.
The machines behind those processes.
A representative register of tooling, moulding and reliability equipment on site. Brand and model shown are the installed units; line allocation is confirmed per programme.
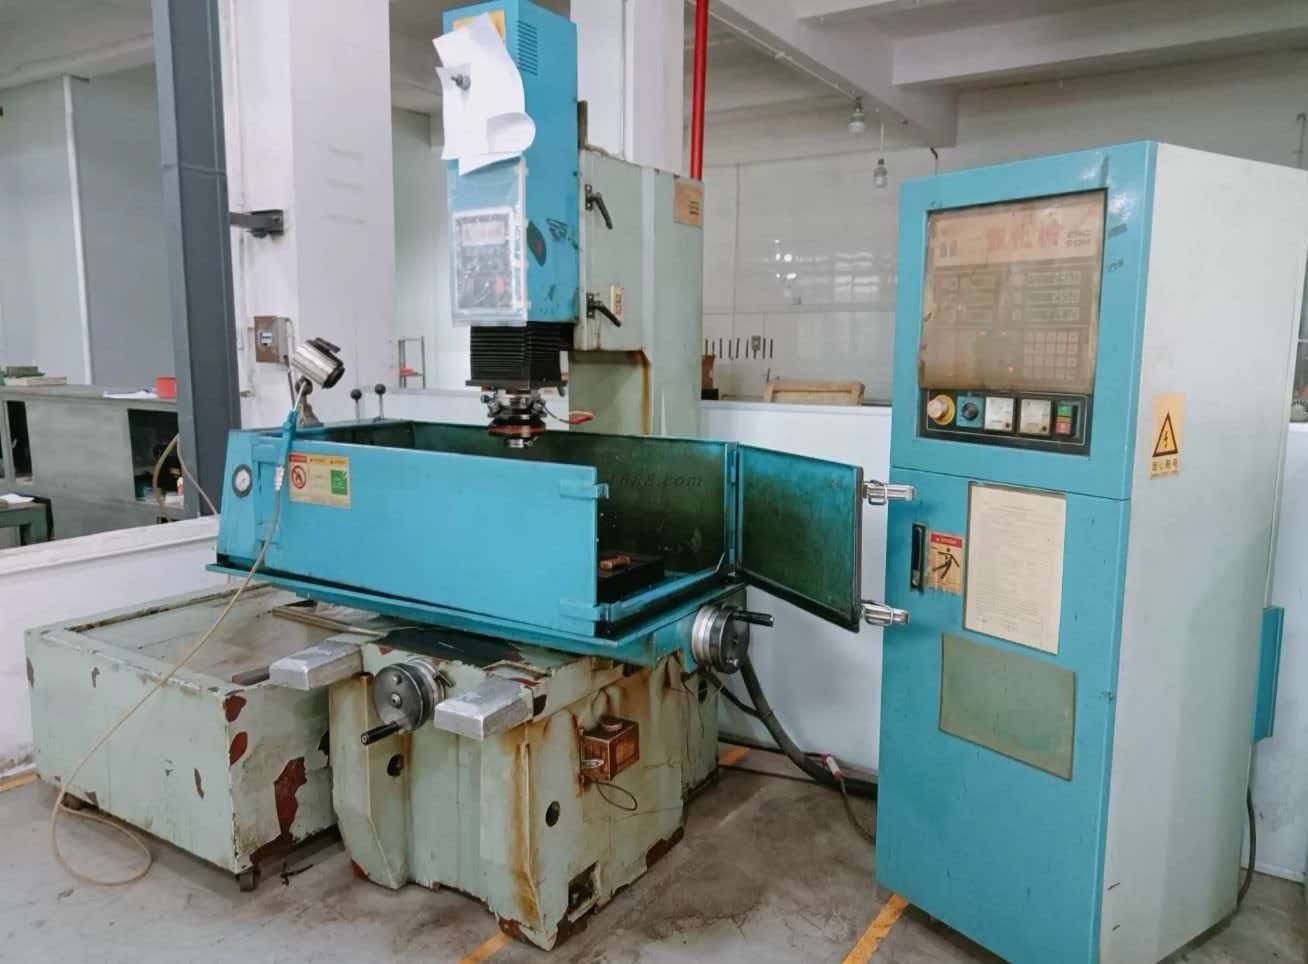
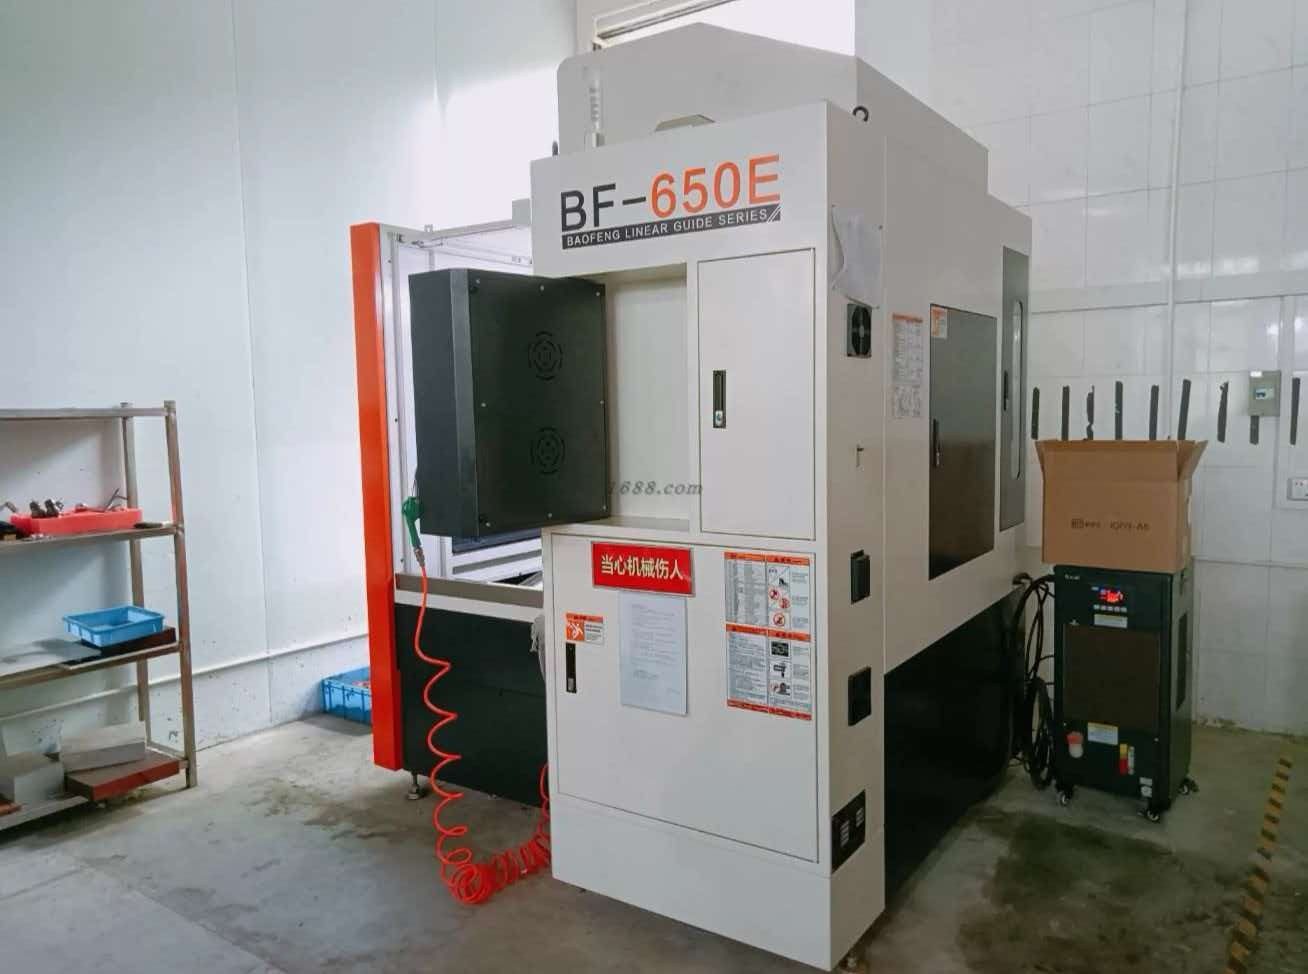
How a defect is supposed to be caught.
Three inspection gates, one traceability chain, and a written corrective action whenever a batch fails. Buyers who audit us usually start here.
Inspection gates
- IQC
- Incoming inspection on all component lots
- IPQC
- In-line checks at SMT, lamination and assembly
- OQC
- 100% functional test · AQL 2.5 final inspection
- Third-party
- SGS, Bureau Veritas, Intertek or TÜV on request
Traceability & corrective action
- Batch records
- Component lots tied to work order and date code
- Unit records
- Serial numbers retained for production batches
- Failure handling
- 8D report issued for any batch-level failure
- RMA
- Fault units returned to the line for root-cause analysis
Engineering & development
- Industrial and mechanical design, working from your ID or a joint design pass
- Electronics, sensor integration and antenna tuning
- Firmware, algorithms and companion-app builds
- In-house sample shop — CNC and 3D printing for fast iterations
- Test and validation plan written per programme, not reused from a template
Tooling ownership
- Tooling paid for by you is your property, held on site and used only for your orders
- Tooling is marked with your programme reference and inventoried
- Maintenance and storage included for the life of the programme
- Transfer or release of tooling agreed in writing at the start, not at the end
Finished-goods warehouse.
Cartoned, zone-coded stock and pallet racking for consolidated container loading. Third-party brand marks on customer-owned cartons are masked in public versions of these photos.
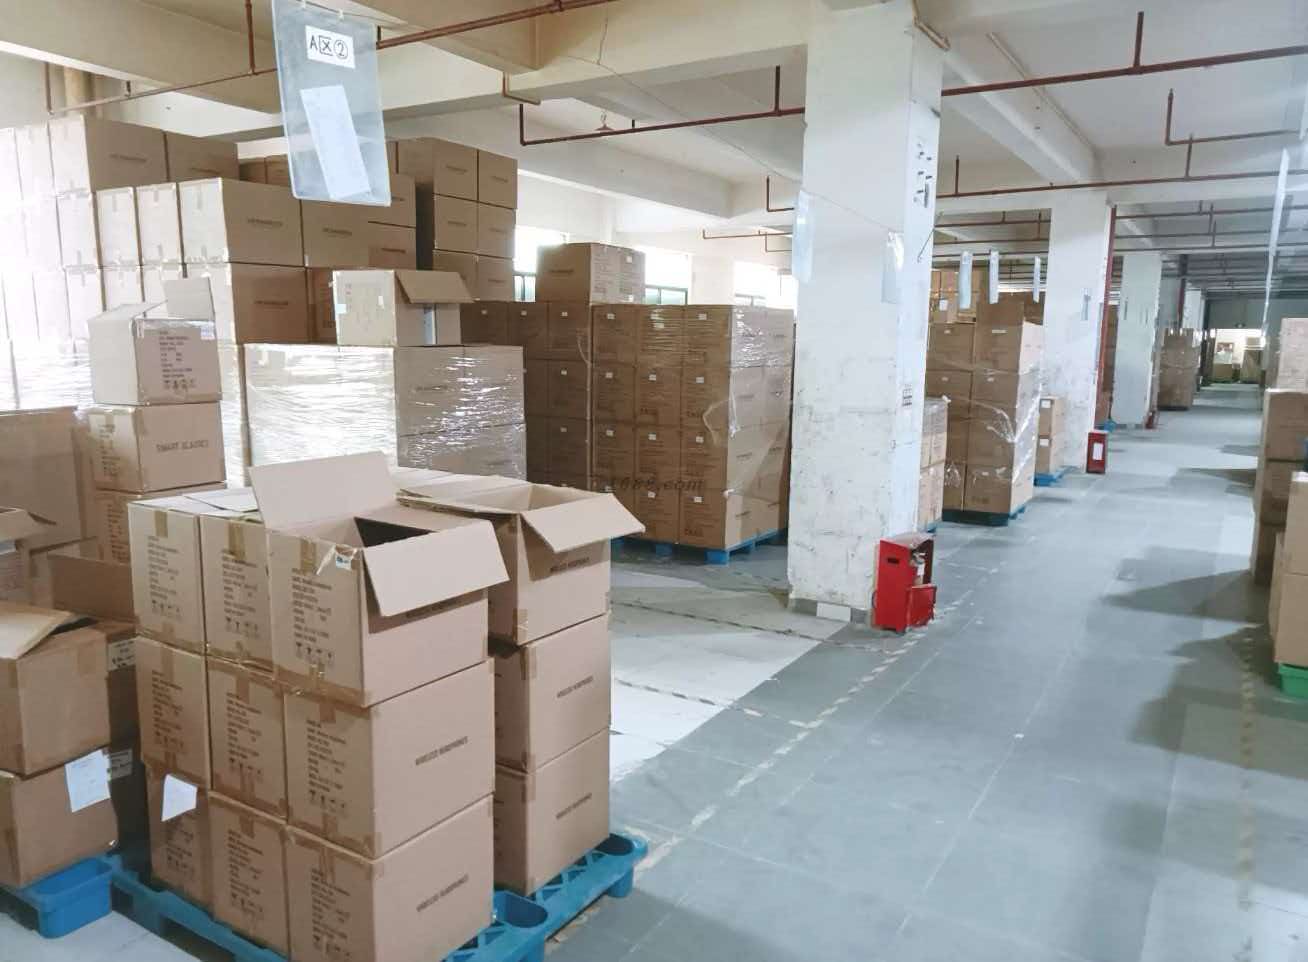
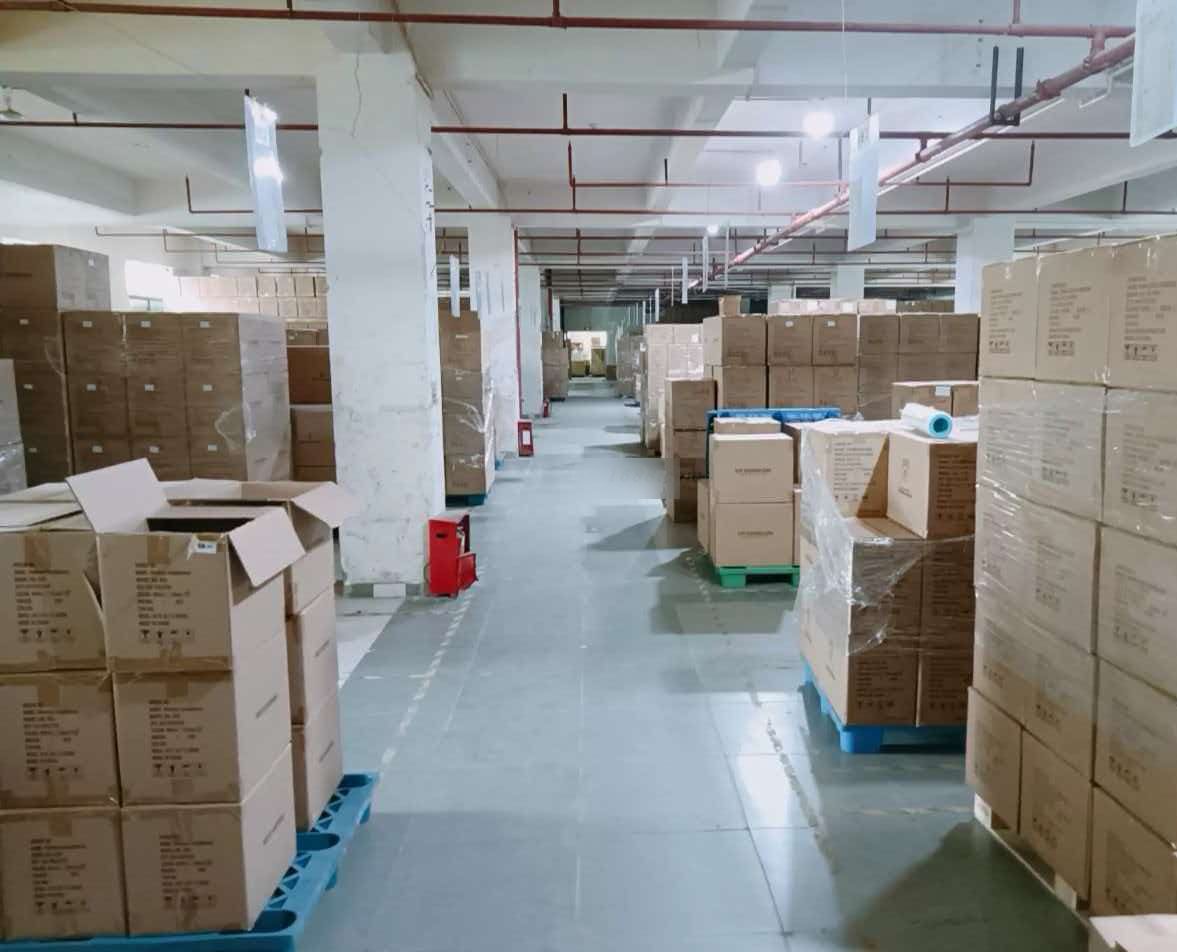
Customer-specific labels and third-party trademarks are removed or obscured before any photo is used in customer-facing material.
Certification is a process, not a sticker.
Product certificates are handled per platform and per market. On top of that, the site itself carries management-system and social-compliance certification — which is what a buyer audit actually checks first.
Quality management
Documented process control across incoming, in-process and outgoing inspection, with corrective action records.
Environmental management
Covers plating and moulding waste handling — the processes buyers ask about most on a site audit.
Occupational health & safety
Worker safety management on the production floor, verified as part of the annual surveillance audit.
Social compliance
Social audit covering working hours, wages, safety and grievance mechanisms — required by most European retail buyers.
Certificates are issued to the legal entity that operates the site. If your procurement process needs the full certificate with the entity name and registration number, we share it during supplier qualification under NDA, together with the current audit report and the site licence. Ask for the qualification pack and it arrives as one document set, not as screenshots.
Come and look at it yourself.
A site visit answers more questions in two hours than a month of email. We arrange them as a standard part of supplier qualification.
Buyer visits
Production floor, sample shop, test area and warehouse walk-through. Two weeks' notice is enough; we will prepare a programme for your visit.
Third-party audits
SGS, Bureau Veritas, Intertek or TÜV can be commissioned by you at any point, including unannounced inspections on live orders.
Remote walkthrough
If travel is not practical, we run a live video walkthrough of the line producing your programme, with your questions answered as it happens.
An NDA is signed before process documentation, tooling drawings or programme records are shared. Your template or ours.
What buyers ask before they book a visit.
Can we visit the production site?
Which audits do you hold, and will you accept ours?
Who owns the tooling we pay for?
Can you run a small pilot production before a full order?
What happens if a production batch fails inspection?
Can you handle the packaging and labelling too?
Do you produce for other brands on the same lines?
Ask for the supplier qualification pack.
Tell us what you need to see — certificates, audit reports, capacity statement, tooling inventory or a visit date — and we will send the document set or propose a programme.
- Sales
- [email protected]
- WhatsApp / WeChat
- +86 000 0000 0000
- Address
- Bao'an District, Shenzhen, Guangdong, China
- Business hours
- Mon–Sat, 09:00–18:00 (GMT+8)